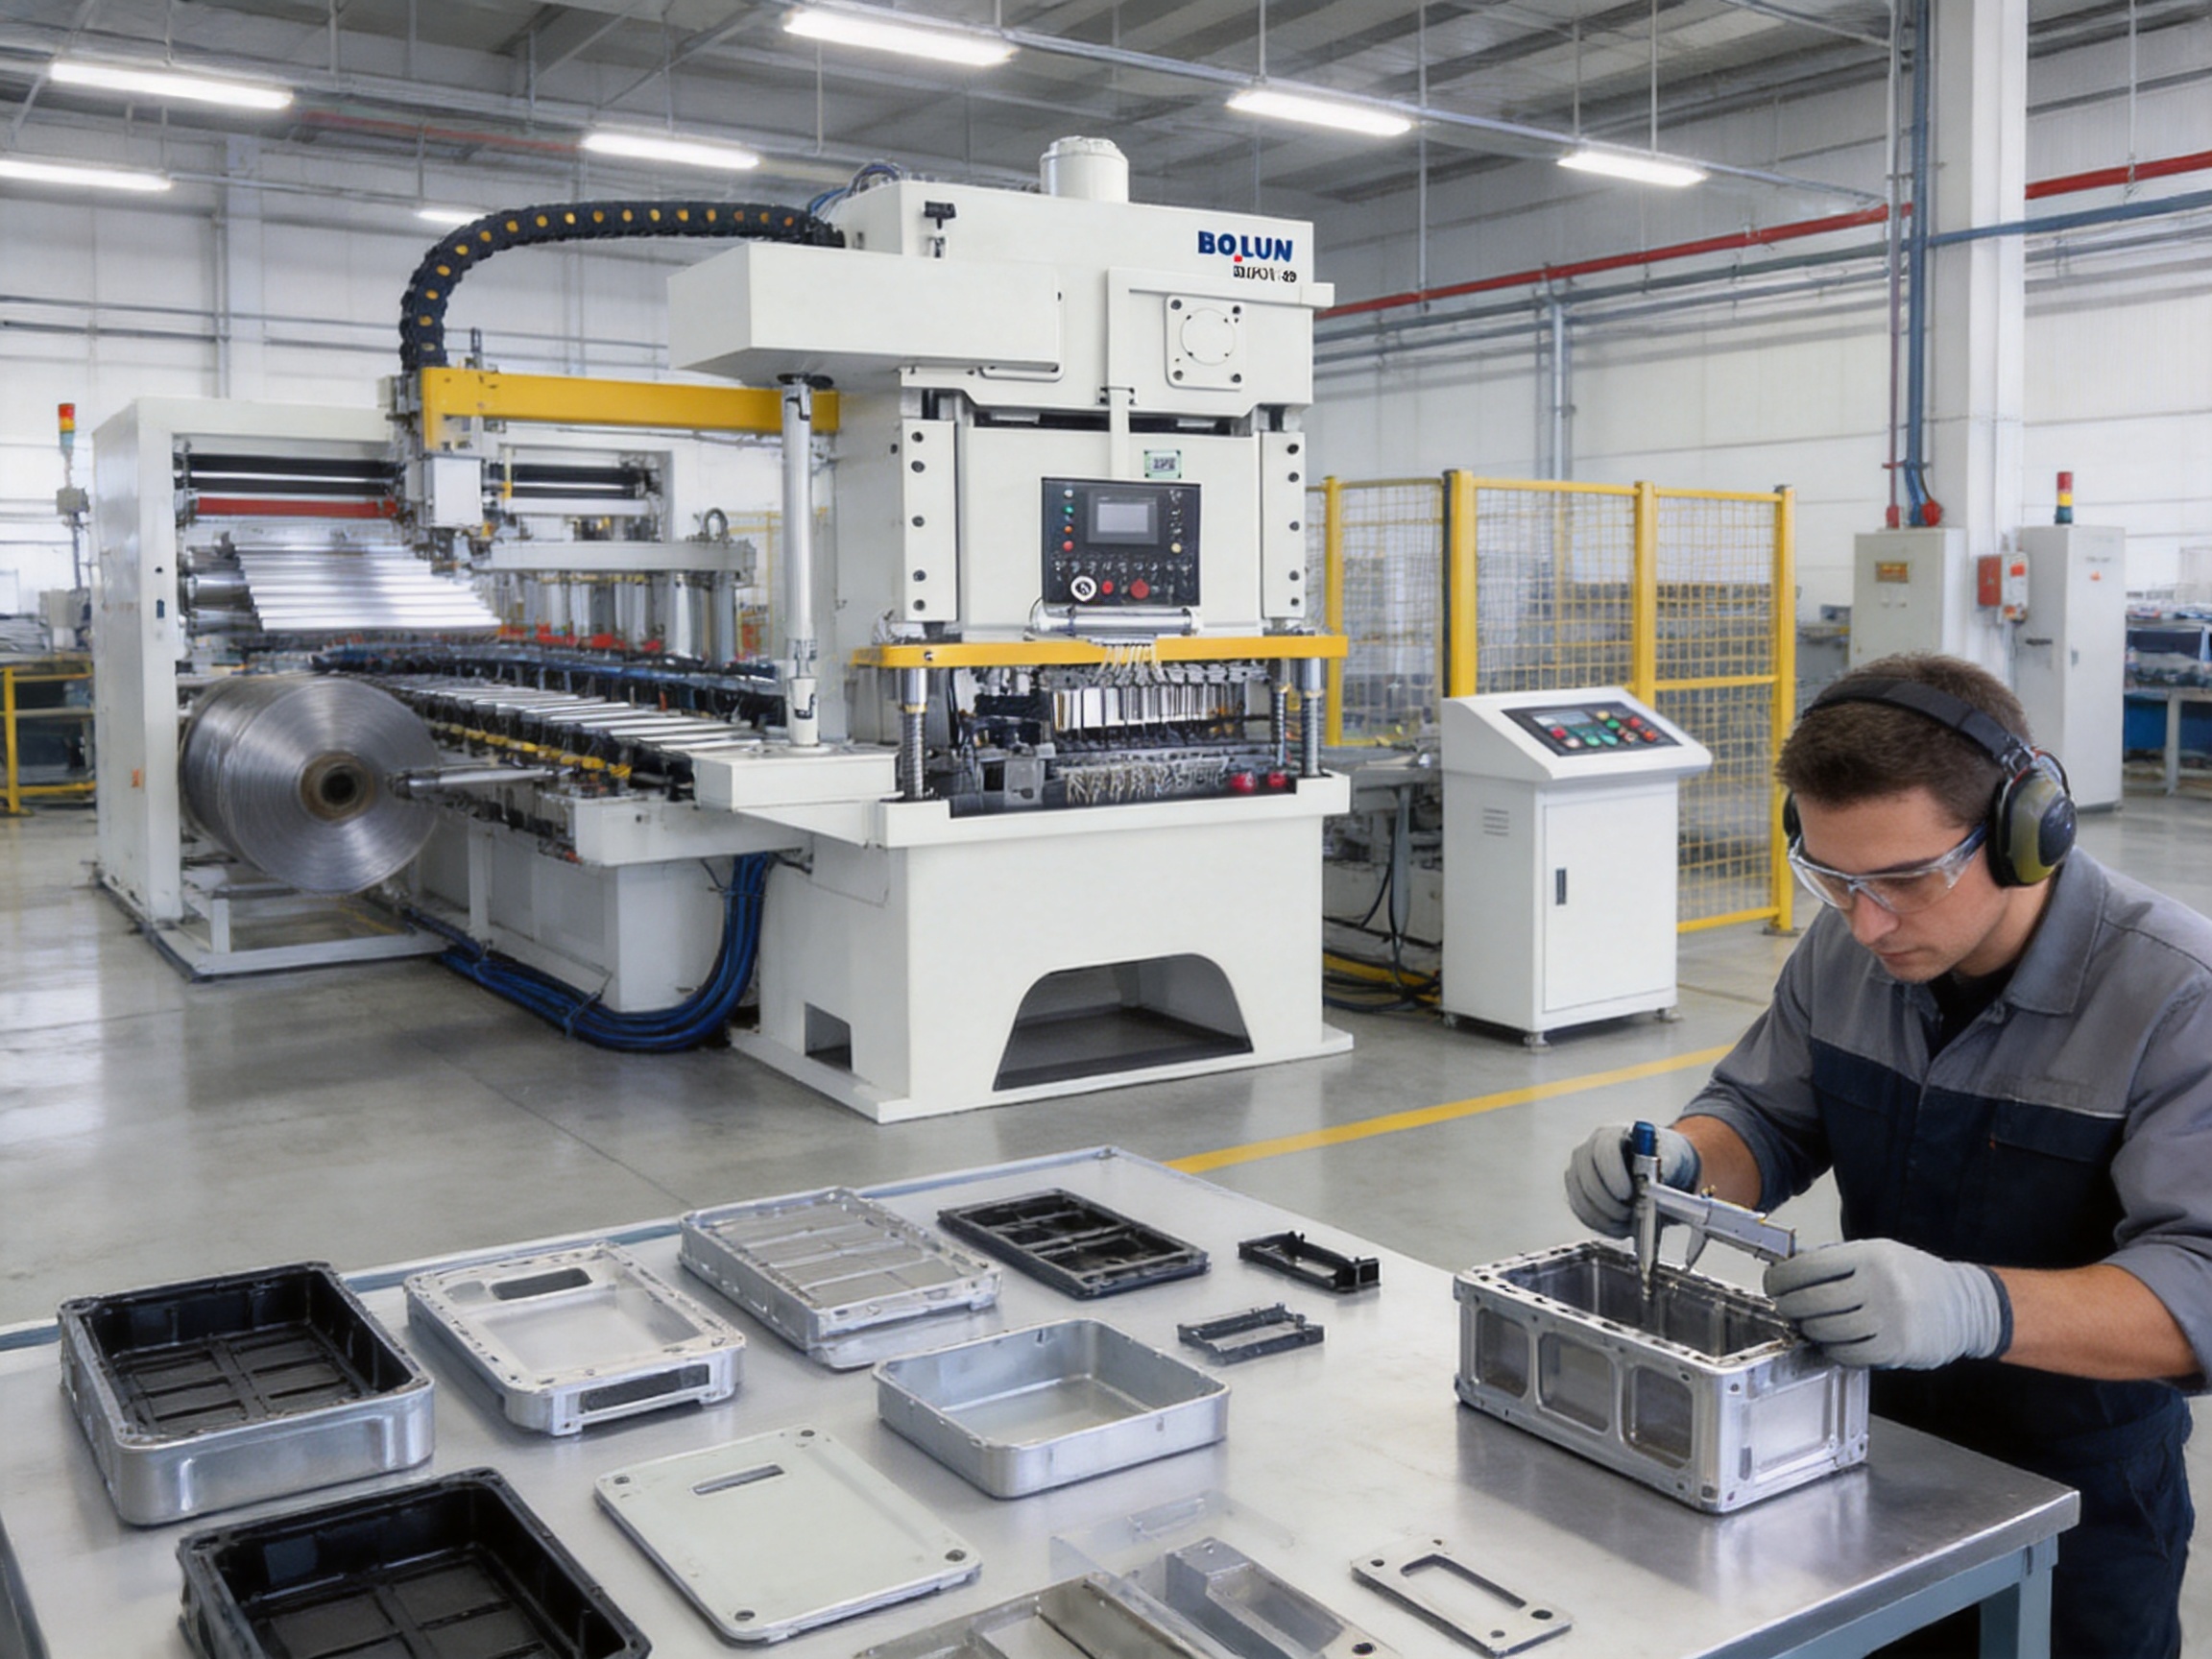
Modern battery manufacturing requires forming equipment that combines high force, accurate motion, structural rigidity, reliable lubrication, and flexible tooling capability. Battery housings, covers, trays, cases, and related energy-storage components often require deep drawing, progressive forming, piercing, trimming, embossing, and other operations that must be performed consistently over long production cycles. A press selected for this work must therefore deliver more than nominal tonnage. It must maintain alignment, absorb forming loads, support large dies, provide stable operating speeds, and adapt to changing product specifications.
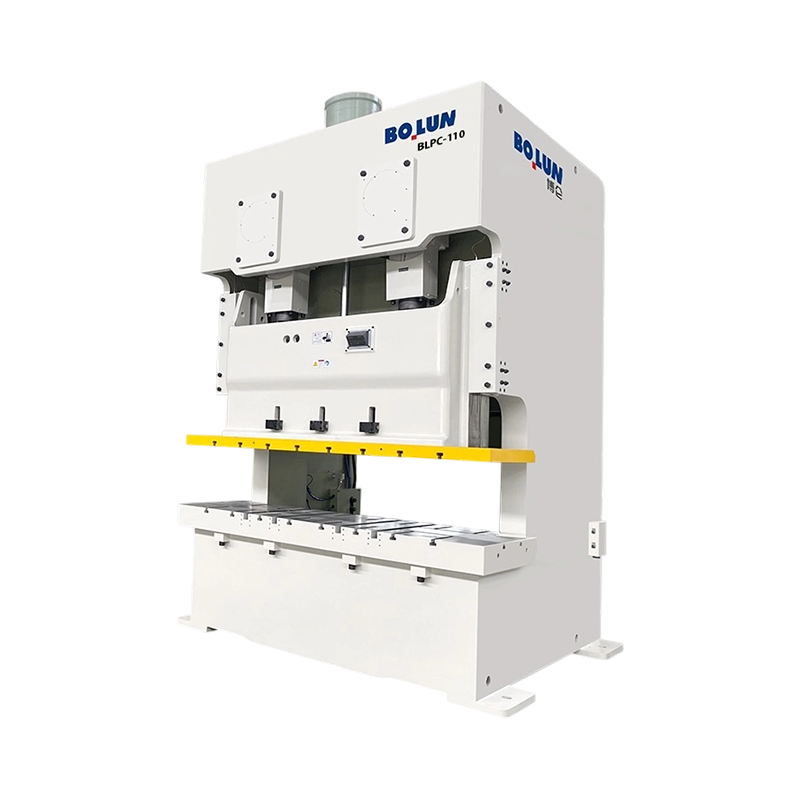
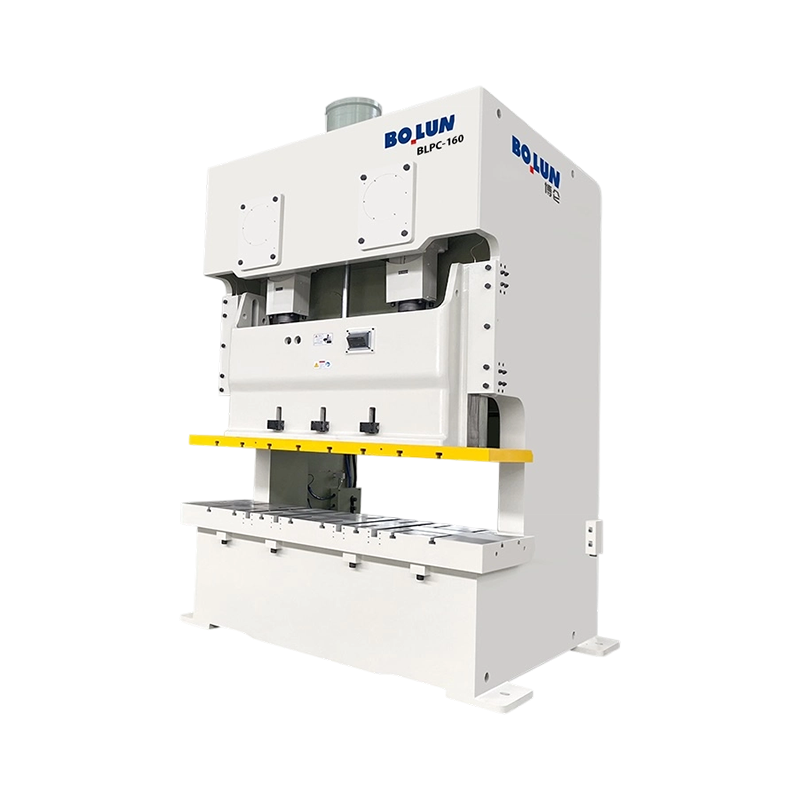
The BLPC2-80 Multi-Spec High-Precision Open-Type Double-Point Battery Power Press is designed for these requirements. With a nominal capacity of 800 kN, a slide stroke of 180 mm, a worktable measuring 1600 × 610 mm, and a maximum die height of 320 mm, it provides a balanced combination of force, working envelope, speed, and tooling flexibility. Its open-type double-point structure supports broad forming applications while helping distribute the load across the slide. A high-rigidity steel frame, electric automatic lubrication system, adjustable die height, and robust drive system further contribute to dependable production performance.
This article examines the machine’s design, operating advantages, specifications, application value, manufacturing strengths, and suitability for battery component production. It also explains how the equipment compares with less specialized press solutions and provides practical guidance for selection, installation, tooling, maintenance, and process planning.
The rapid expansion of electric vehicles, energy-storage systems, portable electronics, and industrial power equipment has increased demand for accurately formed metal battery components. Battery cases and housings are commonly manufactured from materials such as aluminum, steel, stainless steel, and other alloys selected for strength, conductivity, corrosion resistance, weight, or thermal performance. These materials must be formed without excessive cracking, wrinkling, distortion, or dimensional variation.
A battery housing may appear simple, but its production can involve demanding combinations of depth, corner radius, wall thickness, flatness, and surface quality. The forming process must also accommodate holes, flanges, reinforcement features, tabs, ribs, and sealing surfaces. In many cases, several operations are integrated into a progressive die or a transfer arrangement. The press must provide enough capacity for the most demanding stage while retaining sufficient working space for the complete die set.
Press stability is especially important in battery production because dimensional deviations can affect assembly, sealing, electrical insulation, thermal management, and final product safety. A press with insufficient rigidity may experience deflection under load. Excessive deflection can lead to uneven forming, premature die wear, inconsistent clearances, and variations between parts. A properly engineered high-precision press helps reduce these risks by maintaining a more stable relationship between the slide, die, worktable, and frame.
Production efficiency is another central consideration. Battery component manufacturers often operate with high output targets and must control scrap rates carefully because material costs, tooling costs, and downstream assembly expenses can be significant. A press that allows fast but controlled cycling, quick die adjustment, easy access to the work area, and dependable lubrication can support a lower total production cost over its service life.
The BLPC2-80 is an open-type double-point battery power press developed for demanding metal forming applications. Its 800 kN nominal capacity places it above lighter general-purpose presses while keeping the machine suitable for a broad range of medium-to-large battery component dies. The 180 mm slide stroke provides additional forming depth compared with smaller models, making the machine appropriate for deeper housings and specialized energy-storage parts.
The double-point configuration uses two connection points between the drive mechanism and the slide. This arrangement helps distribute forming loads across a wider area than a single-point design. For large dies or workpieces with broad forming surfaces, load distribution can support better slide guidance and improved resistance to twisting. It is particularly valuable when the tooling has multiple forming stations or when the workpiece requires consistent force across its width.
The machine’s 1600 × 610 mm worktable offers a large mounting area for dies, blank holders, progressive tooling, and auxiliary components. The 320 mm maximum die height expands the range of tools that can be installed. Together, these dimensions provide useful flexibility for manufacturers producing several battery housing sizes or changing between different energy-storage product families.
The high-rigidity steel frame is intended to minimize vibration and deformation during operation. Frame rigidity is directly connected to forming accuracy, die life, and operating noise. When the frame and slide remain stable under load, the die can work with more predictable clearances and the finished components can maintain more consistent dimensions.
An integrated electric automatic lubrication system supplies lubricant to key moving areas at scheduled intervals. This reduces dependence on manual lubrication routines and helps ensure that critical components receive appropriate lubrication during production. Automated lubrication can also support more consistent maintenance practices across multiple shifts.
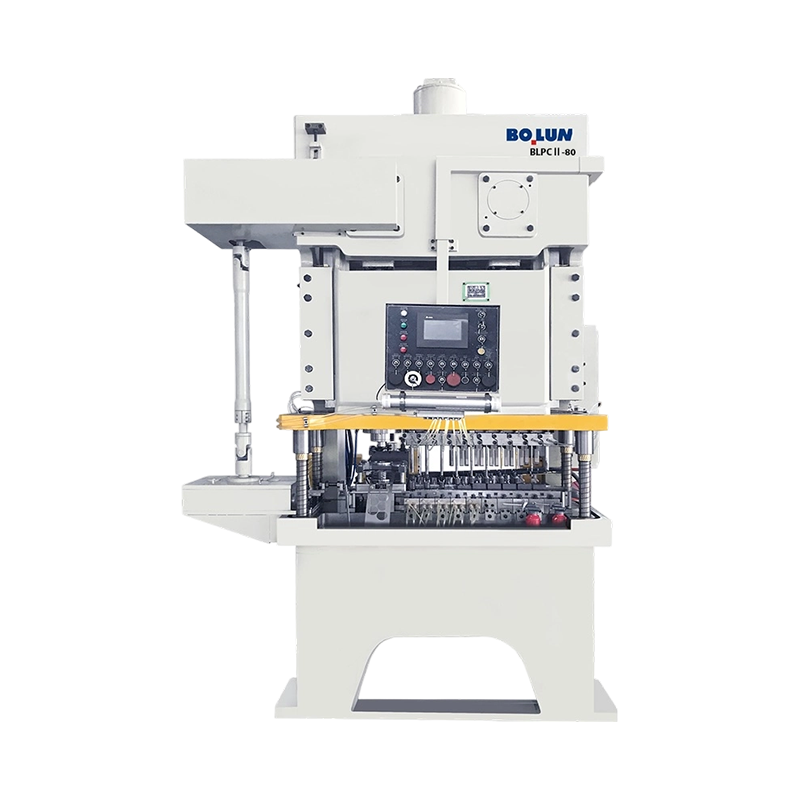
BLPC2-80 Multi-Spec High-Precision Open-Type Double-Point Battery Power Press
The following table summarizes the principal data associated with the BLPC2-80 model and places it within the related BLPC II product range. The BLPC II-63 and BLPC II-110 models are included for comparison, while the BLPC II-80 column represents the machine corresponding to the product described in this article.
| Specification | Unit | BLPC II-63 | BLPC II-80 | BLPC II-110 |
|---|---|---|---|---|
| Nominal capacity | kN | 630 | 800 | 1100 |
| Nominal pressure stroke | mm | 5 | 5 | 5 |
| Slide stroke | mm | 140 | 180 | 190 |
| Strokes per minute | S.P.M. | 50–80 | 45–75 | 35–70 |
| Maximum die height | mm | 280 | 320 | 480 |
| Die height adjustment | mm | 50 | 80 | 90 |
| Worktable size | mm | 1300 × 550 × 120 | 1600 × 610 × 130 | 1970 × 680 × 130 |
| Slide bottom size | mm | 1200 × 500 × 70 | 1450 × 520 × 70 | 1800 × 580 × 70 |
| Side opening | mm | 250 × 120 | 300 × 140 | 320 × 180 |
| Throat depth | mm | 285 | 310 | 350 |
| Distance between columns | mm | 1000 | 1200 | 1550 |
| Height of working face | mm | 940 | 957 | 1085 |
| Maximum weight | kg | 360 | 450 | 690 |
| Air pressure | MPa | 0.55 | 0.55 | 0.55 |
| Power supply | V/Hz | Three-phase 380 V, 50 Hz | Three-phase 380 V, 50 Hz | Three-phase 380 V, 50 Hz |
| Main motor | kW × poles | 7.5 × 4 | 11 × 4 | 15 × 4 |
The BLPC II-80 configuration occupies a practical position within the range. The 630 kN model is suitable for applications requiring lower forming force and a smaller working area, while the 1100 kN model addresses larger or heavier-duty operations. The 800 kN version offers a useful intermediate capacity with an enlarged worktable, longer stroke, and greater die-height capability than the smaller model.
Nominal capacity is one of the first specifications considered when selecting a power press. The BLPC2-80 provides 800 kN of nominal force, equivalent to a substantial forming capability for battery cases, covers, trays, structural plates, and other stamped parts. This capacity gives manufacturers additional process margin when compared with smaller presses that may operate close to their maximum rating.
Operating with a suitable force margin is important for several reasons. First, it reduces the risk that variations in material thickness, hardness, lubrication, or die condition will exceed the practical capability of the press. Second, it allows the manufacturer to consider future product development without immediately replacing the machine. Third, it can improve machine longevity when the regular production load remains below the maximum capacity rather than constantly approaching it.
The correct capacity must always be determined from actual process calculations. Required press force depends on material grade, thickness, blank size, forming method, cutting perimeter, friction, draw ratio, number of simultaneous operations, and die design. The 800 kN rating should therefore be evaluated together with the complete force curve and the pressure point of the intended tooling. Nevertheless, for many medium-to-large battery component applications, this capacity provides a strong foundation.
The 180 mm slide stroke is a significant feature of the BLPC2-80. Compared with the 140 mm stroke of the related 630 kN model, the longer stroke provides more vertical travel for forming operations. This can be beneficial when producing deeper housings, components with pronounced flanges, or parts requiring a greater distance between the upper and lower tooling positions.
A longer stroke can also increase process flexibility. It may provide additional space for part loading and unloading, improve access during die development, and accommodate forming sequences that cannot be completed effectively within a shorter movement. In deep drawing and complex forming, sufficient travel is essential for controlling the motion of the blank holder, punch, and forming surfaces.
Stroke length should not be considered in isolation. The best result depends on coordination between stroke, slide speed, die height, shut height, material flow, and the timing of auxiliary systems. The BLPC2-80 combines its 180 mm stroke with a 320 mm maximum die height and 80 mm die-height adjustment, creating a more adaptable platform for different tooling configurations.
The 1600 × 610 mm worktable is designed to support larger dies and broader production layouts. A generous worktable can simplify die mounting, provide room for guide components, and accommodate multiple forming stations. It also gives tooling engineers more freedom when arranging blank feeding, part transfer, scrap discharge, sensors, and other process equipment.
The 130 mm table thickness contributes to a stable base for die installation. A stable table is important because uneven support or localized deflection can influence die alignment and finished-part quality. Before production, the die and bolster arrangement should be checked carefully to ensure that the actual load distribution remains within the machine and tooling limits.
The slide bottom measures 1450 × 520 × 70 mm on the BLPC II-80 configuration. This broad slide mounting surface complements the worktable and supports double-point tooling arrangements. The 1200 mm distance between columns also offers a useful working width for battery-related components and multi-cavity dies.
The maximum die height of 320 mm and adjustment range of 80 mm help the machine accommodate dies with different closed heights. This is particularly useful for manufacturers that operate several product lines or use progressive tooling with varying station arrangements. A flexible die-height range can reduce the need for extensive machine modification when changing jobs.
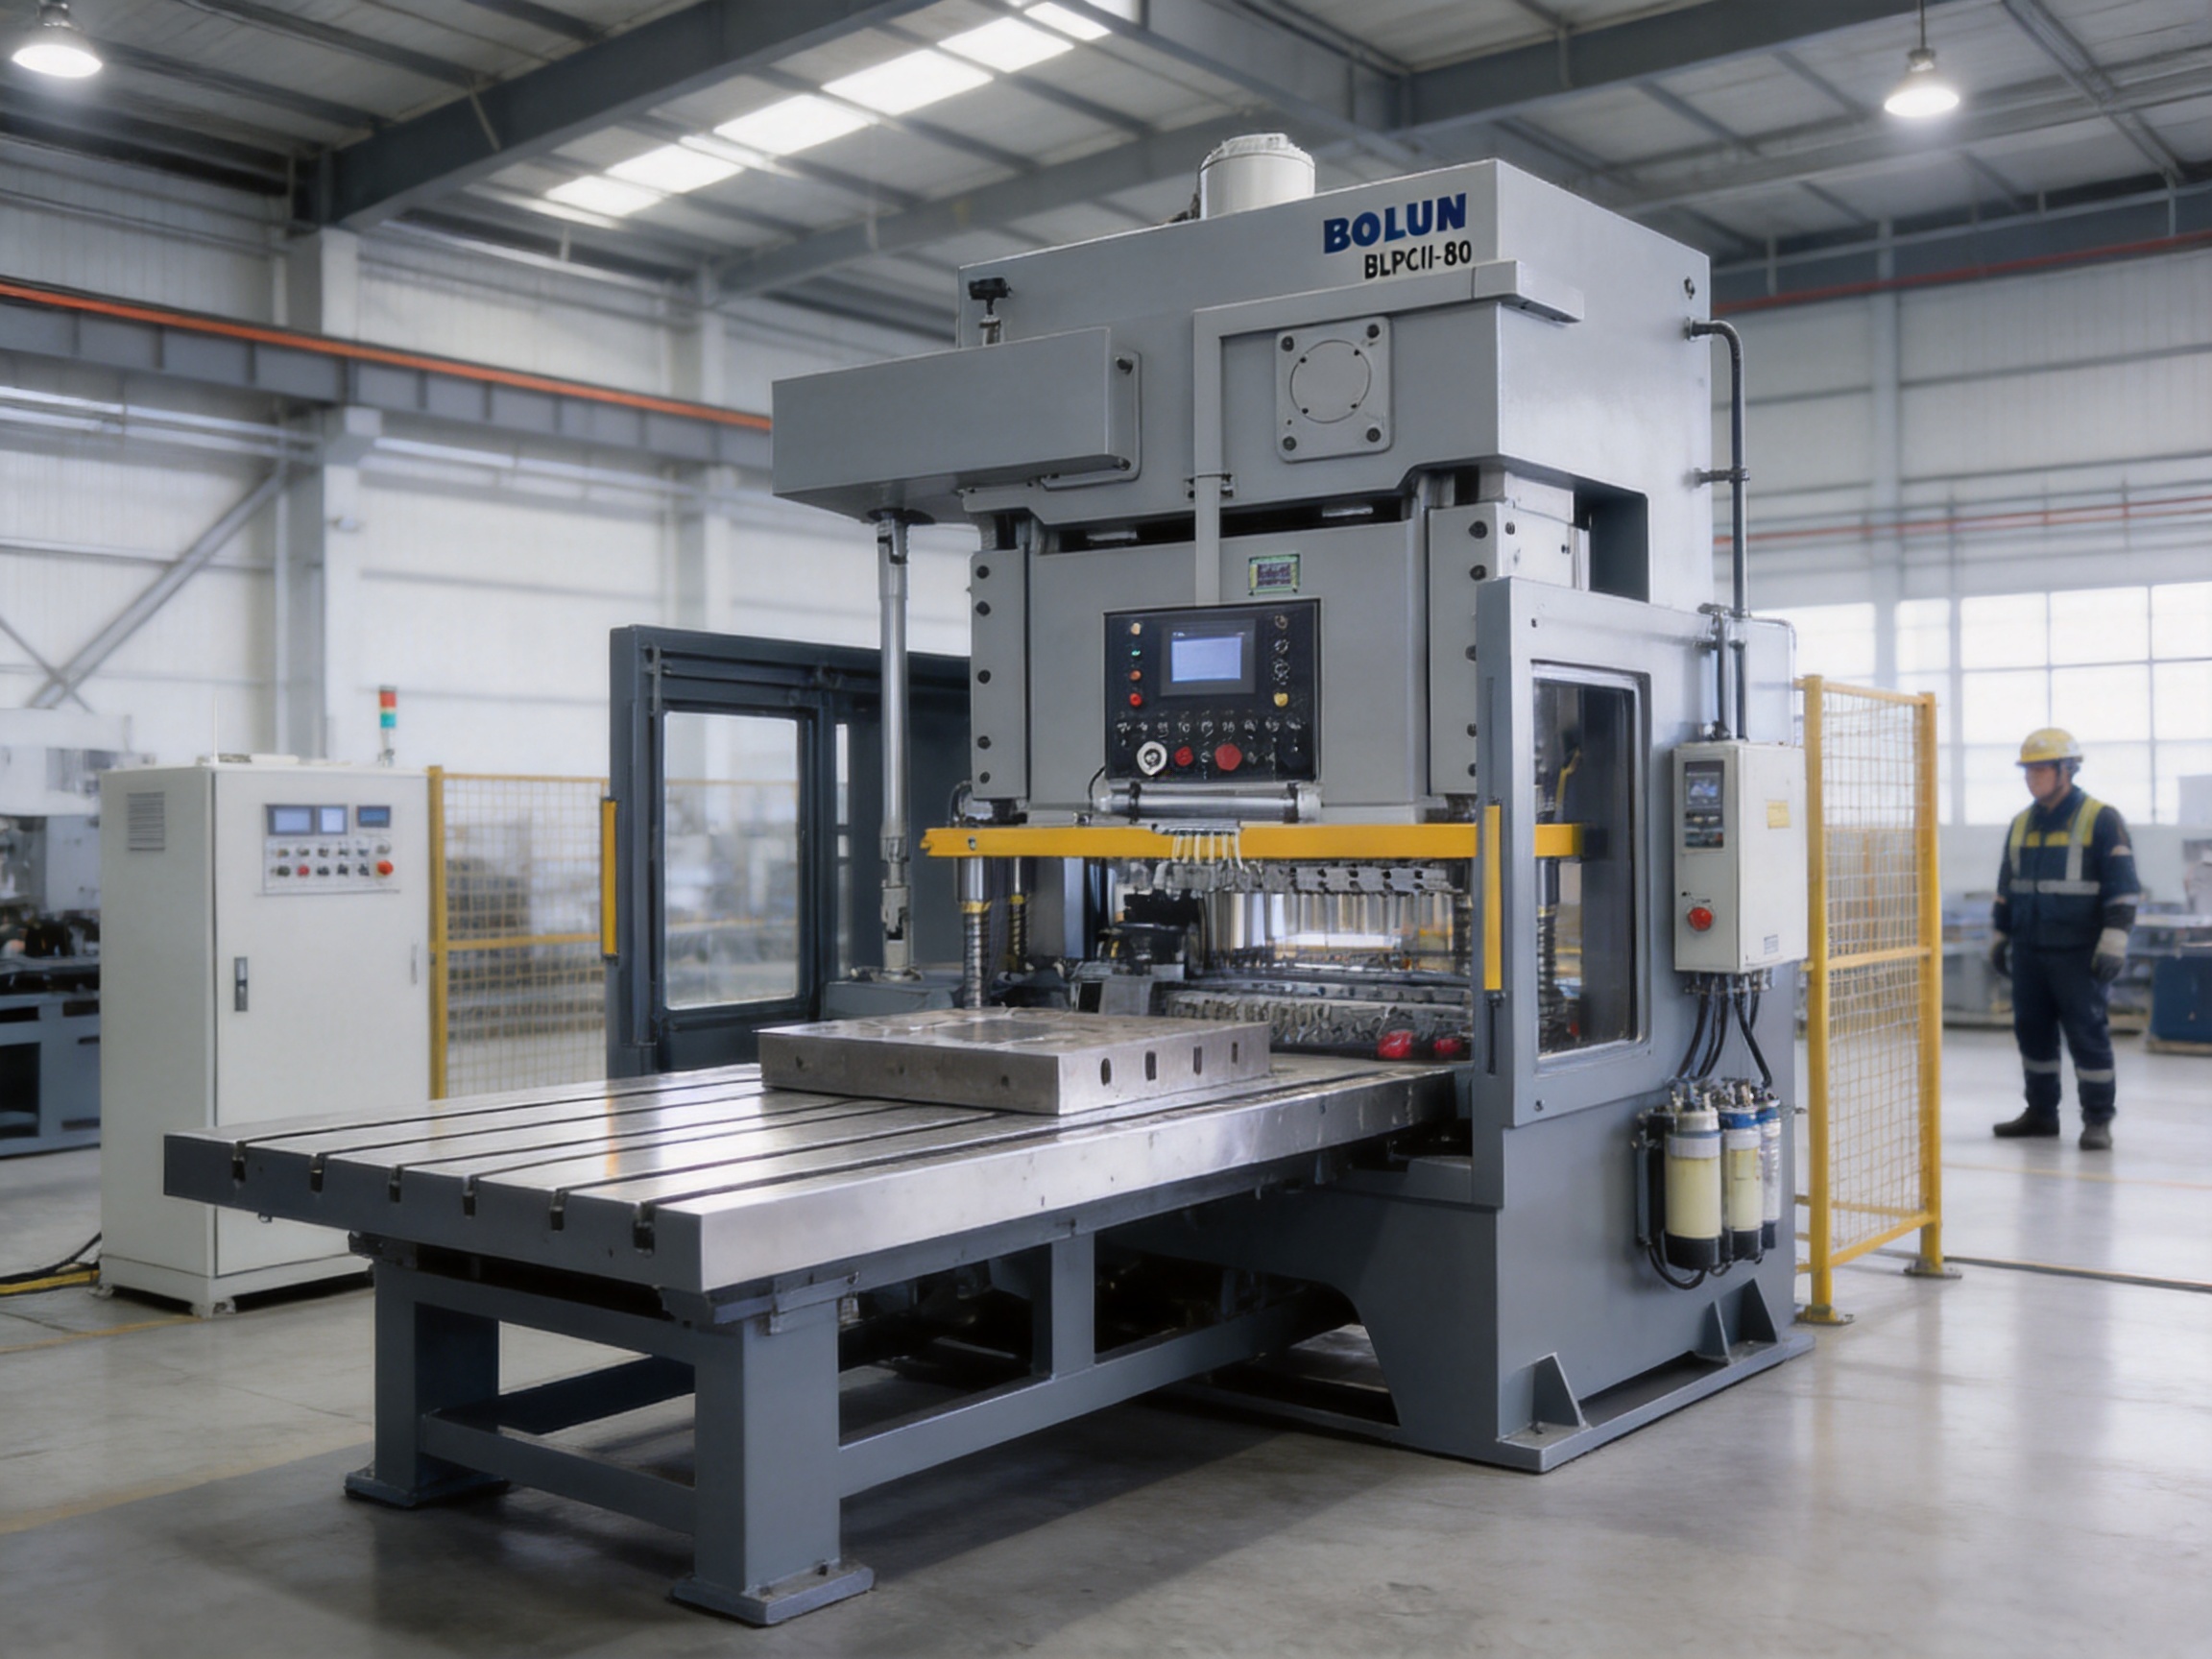
The double-point design is one of the machine’s most important advantages for wide or unevenly loaded dies. In a single-point press, the force is introduced through one central connection. That arrangement can be effective for many applications, but wide tooling or off-center loads may create a greater tendency toward slide tilting. A double-point press introduces force through two points, helping distribute the load across the slide.
Improved load distribution can support more uniform die engagement, especially when the forming operation extends over a broad work area. It may also help reduce angular movement and improve repeatability during production. These benefits are valuable in battery component manufacturing, where parallelism, flatness, flange accuracy, and consistent wall geometry often influence downstream assembly.
Double-point architecture is not a substitute for correct die design or proper setup. The die must still be balanced, the load must remain within the recommended working zone, and the slide guides must be maintained. However, the structure provides a stronger foundation for these requirements than a compact single-point design intended primarily for smaller parts.
The open-side construction further improves accessibility. Operators and maintenance personnel can generally reach the work area more easily than with a fully enclosed frame. The side opening listed for the BLPC II-80 is 300 × 140 mm, which can help with visual inspection, die servicing, and the arrangement of certain auxiliary devices. Access should always be managed according to the applicable safety system and guarding requirements.
Frame rigidity has a direct influence on the long-term performance of a mechanical press. During forming, the frame, slide, table, connecting components, and die absorb substantial forces. If these structures flex excessively, the press may experience variation in shut height, uneven pressure distribution, vibration, and reduced dimensional consistency.
The BLPC2-80 uses a high-rigidity steel frame intended to withstand demanding production loads. A rigid frame helps maintain the geometry of the working zone and reduces unwanted movement during the forming cycle. This can support better repeatability, especially in operations where die clearance and tool parallelism are tightly controlled.
Structural rigidity also contributes to die protection. When the press frame responds predictably to load, the tooling is less likely to experience sudden misalignment or uneven contact caused by excessive machine deflection. Reduced vibration may help extend the service life of punches, dies, guide posts, springs, and other wear components.
In practical production, frame performance should be supported by correct foundation design, accurate leveling, proper anchoring, and periodic inspection. Even a well-engineered machine cannot achieve its intended accuracy if it is installed on an unsuitable foundation or operated with an improperly aligned die.
Lubrication is essential to the operation of a power press. Bearings, slides, shafts, gears, joints, and other moving surfaces require the correct lubricant in the correct quantity and at suitable intervals. Inadequate lubrication may lead to friction, heat, accelerated wear, noise, and unplanned downtime.
The BLPC2-80 incorporates an electric automatic lubrication system. This system is intended to deliver lubricant according to a programmed or controlled schedule, reducing reliance on manual application. Automatic lubrication is especially beneficial in multi-shift production, where manual routines may vary between operators or become difficult to perform consistently.
A controlled lubrication system can contribute to more stable machine operation and support predictable maintenance planning. It can also reduce the possibility of missing difficult-to-reach lubrication points. However, automatic lubrication does not eliminate the need for inspection. Operators should monitor lubricant level, pump operation, distribution lines, alarms, leakage, and the condition of lubricated components.
Using the lubricant specified for the press and maintaining clean supply equipment are equally important. Contaminated or unsuitable lubricant can cause damage even when the delivery frequency is correct. A documented lubrication checklist should be included in the plant’s preventive-maintenance program.
The BLPC II-80 is rated at approximately 45–75 strokes per minute. This range allows the machine to support productive cycle times while giving process engineers room to select a suitable speed for the material, die, and forming operation. Higher speed can increase output, but maximum speed is not always the best operating speed for a deep or demanding battery component.
Production speed should be selected after evaluating material flow, lubrication, blank feeding, die cooling if required, part removal, scrap handling, vibration, noise, and quality results. A controlled speed that produces stable parts may deliver a better overall cost than a faster speed accompanied by high scrap or frequent stoppages.
The availability of a speed range also helps manufacturers use one machine for different jobs. Shallow stamping, piercing, and trimming may permit faster operation, while deeper drawing or complex forming may require a slower setting. This versatility is valuable for factories that produce several component types rather than a single high-volume part.
The 11 kW main motor supports the drive system for the BLPC II-80 configuration. Electrical installation should be planned around the specified three-phase 380 V, 50 Hz supply, together with the machine’s starting, control, grounding, and protection requirements. Local electrical regulations and the customer’s plant standards must be confirmed before commissioning.
Battery component manufacturers may compare the BLPC2-80 with small single-point presses, general-purpose open presses, enclosed straight-side presses, hydraulic presses, or larger high-capacity machines. Each alternative has advantages in specific applications, but the double-point battery press offers a balanced combination of features that can be valuable for medium-to-large stamped components.
A smaller single-point press may require less floor space and have a lower initial purchase price. It can be suitable for small covers, brackets, terminals, and simple shallow parts. However, its lower capacity, shorter stroke, smaller table, and single central load path may limit its usefulness for wider or deeper battery housings.
The BLPC2-80 provides greater forming capacity, a longer stroke, a larger worktable, and a double-point structure. These characteristics can reduce the need to divide a component into more production stages or use multiple smaller machines. The result may be a more flexible production platform for growing battery product portfolios.
A general-purpose press may perform many operations, but not every model is optimized for wide tooling, deep housings, or long production cycles. Some basic machines may provide limited die-height adjustment, smaller slide surfaces, less sophisticated lubrication, or lower structural rigidity.
The BLPC2-80 is more closely aligned with applications where forming accuracy, die flexibility, and stable operation are central priorities. Its specifications provide a broader working envelope, and its automatic lubrication system supports a more systematic production environment.
Hydraulic presses are known for controllable force and stroke characteristics and can be advantageous for certain deep-drawing or low-speed forming applications. A mechanical power press, however, can offer high production speed and efficient repetitive cycling for stamping, piercing, trimming, and progressive operations.
The best choice depends on the material, part geometry, force curve, required speed, and process sequence. The BLPC2-80 is particularly suitable when the production plan benefits from a mechanical press’s repeatable high-speed motion and broad die compatibility.
A larger 1100 kN machine provides additional force and a larger working envelope, but it also normally requires greater investment, floor space, power, tooling, and foundation capacity. If the actual production requirement falls within the 800 kN range, selecting a very large machine may create unnecessary operating costs.
The BLPC2-80 can therefore represent a practical middle solution. It offers more capability than the 630 kN model while avoiding the additional scale of the 1100 kN model. The appropriate selection should be based on calculated forming force, die dimensions, product roadmap, and expected utilization.
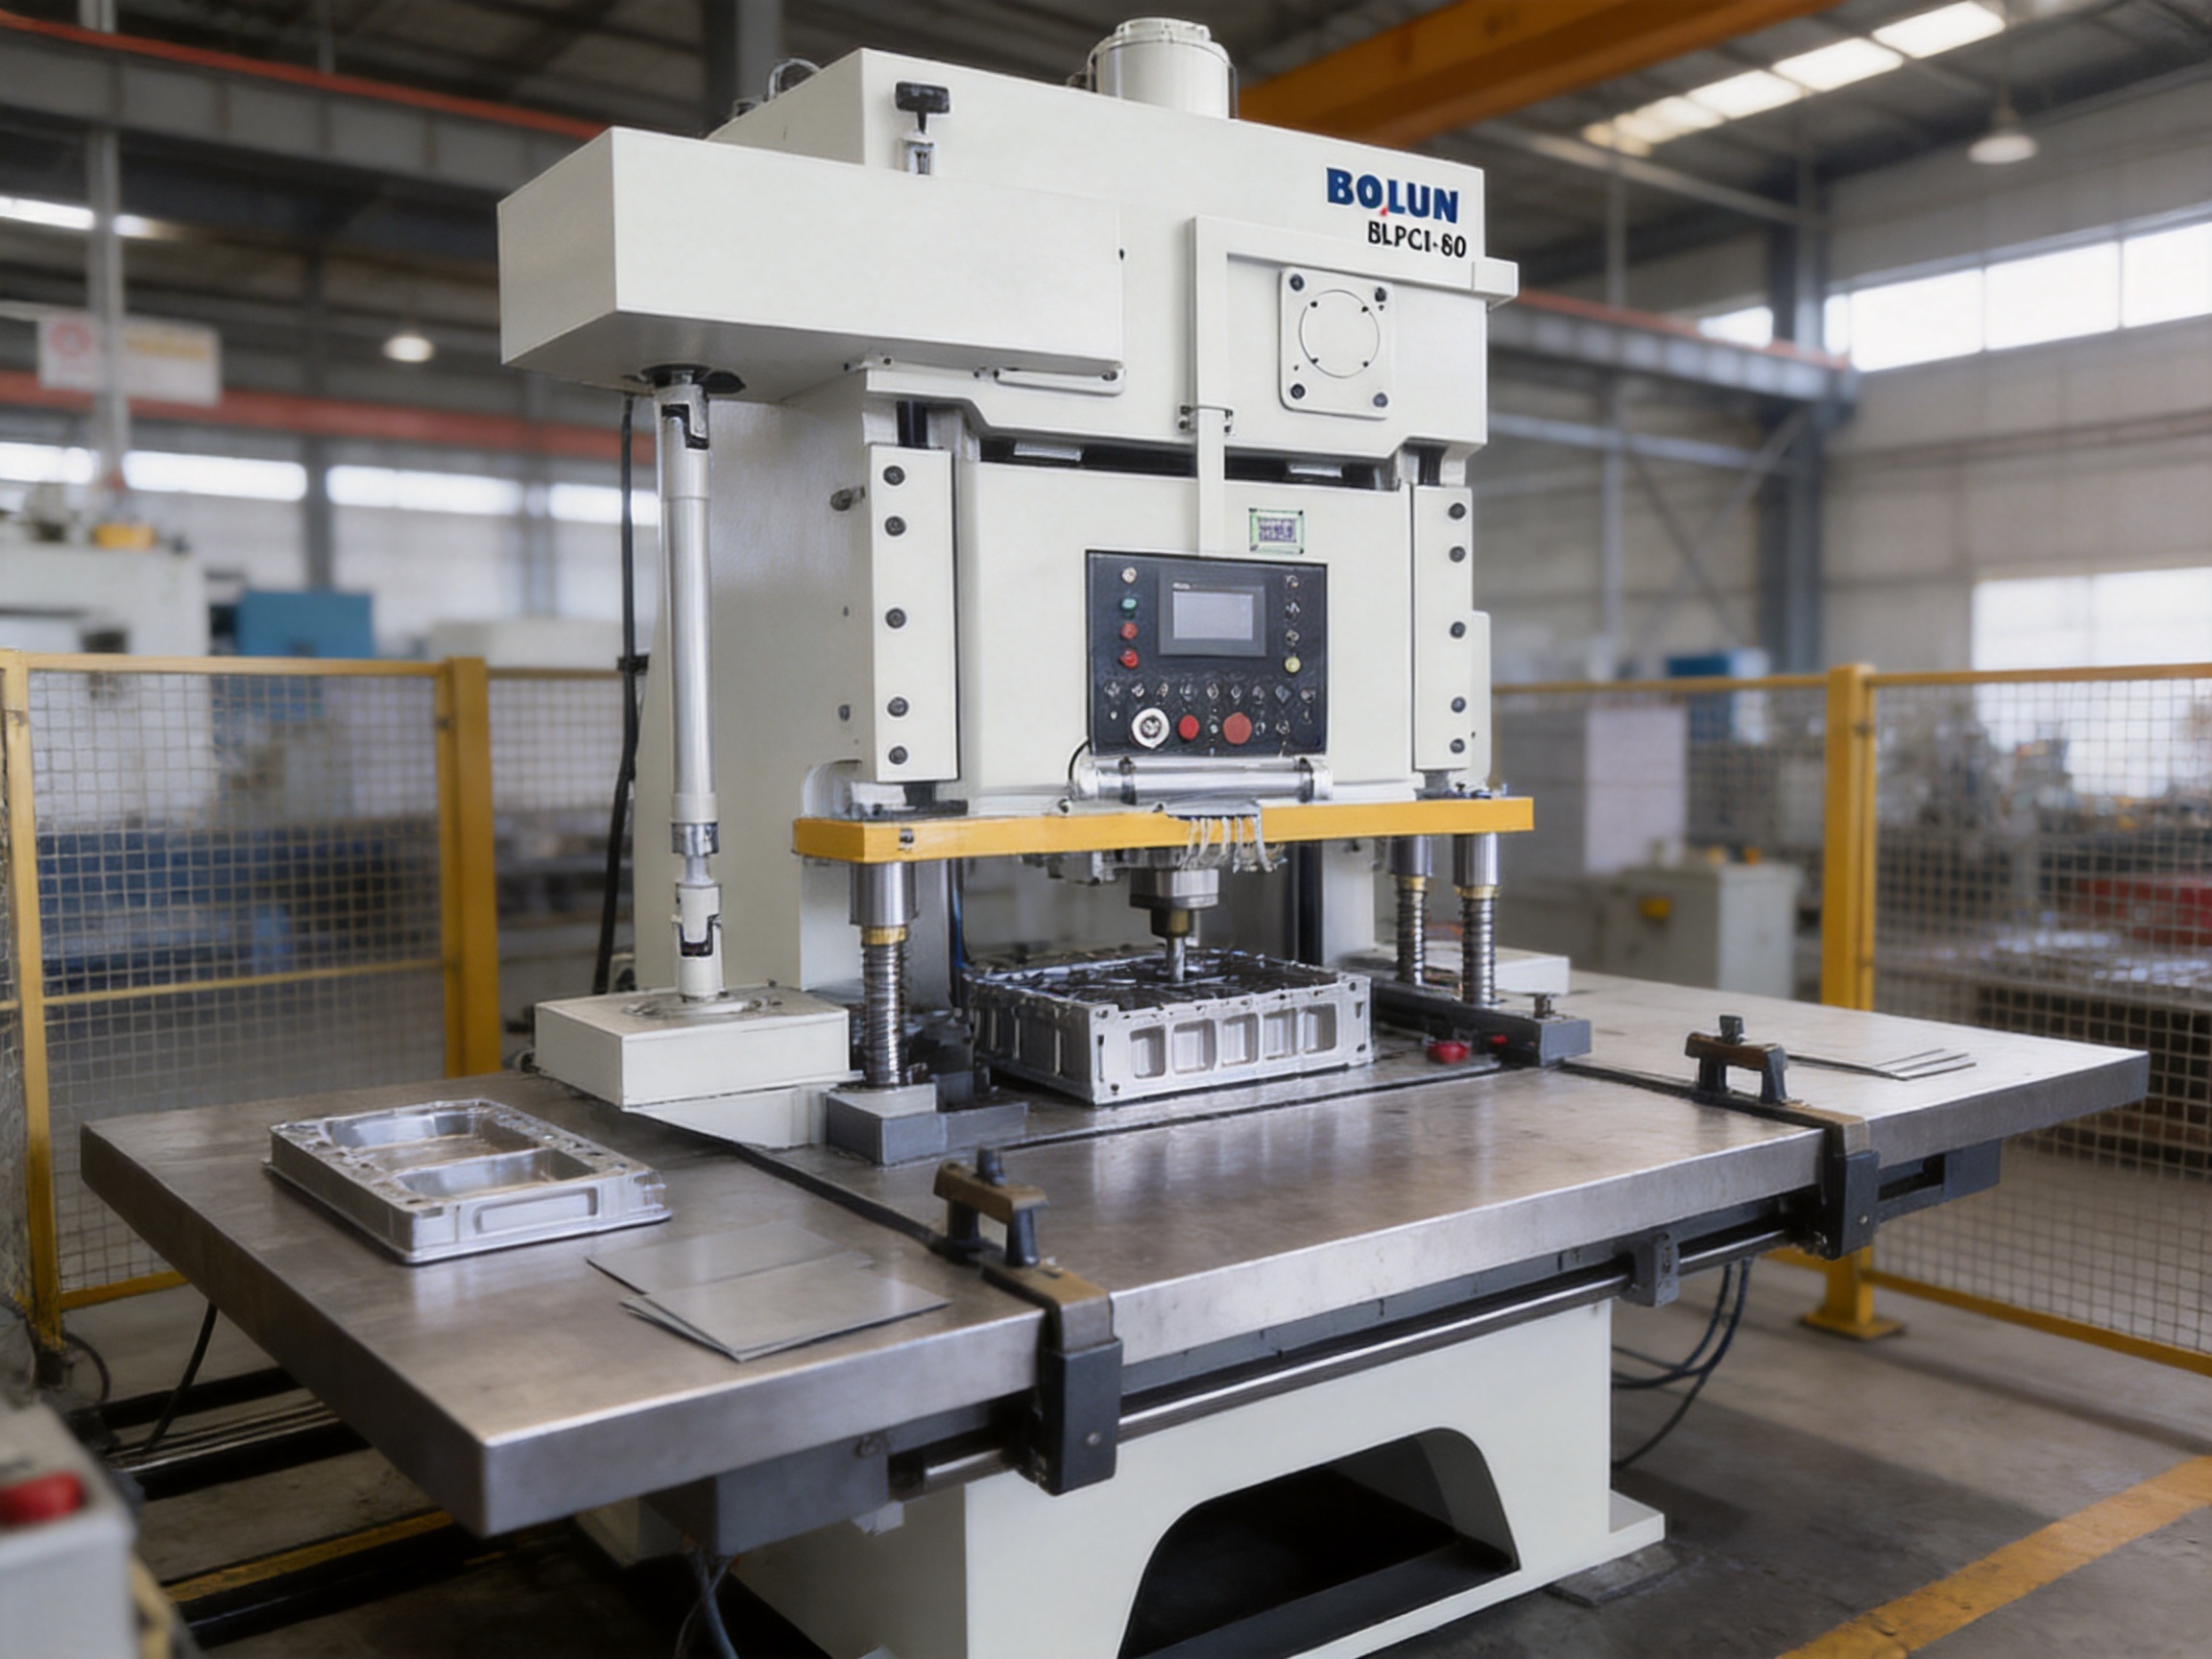
The machine is suited to a range of metal forming applications associated with batteries and energy-storage products. Potential applications include battery housings, battery covers, metal trays, enclosure panels, reinforcement parts, mounting plates, terminal plates, brackets, shielding components, and other formed structural parts.
For cylindrical, prismatic, or pouch-battery systems, the specific component geometry varies considerably. Some parts may be deep and narrow, while others may be wide, shallow, or heavily flanged. The BLPC2-80’s stroke, table size, die height, and double-point structure provide a useful base for tooling adapted to these different geometries.
In energy-storage cabinets and industrial battery systems, stamped metal parts may require larger dimensions and more extensive forming surfaces than portable battery components. The machine’s broad worktable and 1200 mm column spacing can support tooling arrangements for these larger parts, subject to the actual die weight, force distribution, and production method.
Automotive battery components may demand strict repeatability and integration with automated feeding and transfer equipment. The press can be considered for progressive die operations or other automated production systems when the tooling, controls, safety devices, and material handling equipment are engineered as a complete line.
Before production approval, each application should be validated through material testing, die trials, dimensional inspection, forming simulation where appropriate, and endurance production runs. Battery-related parts often have safety-critical or assembly-critical functions, so process qualification should be documented carefully.
The equipment is produced by Zhejiang Bolun High-Precision Machinery Co., Ltd., a Chinese manufacturer focused on high-precision forming equipment. The company combines research and development, design, production, sales, and service. This integrated structure can help coordinate machine design, manufacturing, customization, commissioning, and technical support through a unified organization.
The company reports approximately two decades of experience in machinery manufacturing and has developed capabilities in forging and casting machinery. Its manufacturing approach covers basic design, core component development, precision processing, assembly, inspection, and final delivery. Such vertical coordination is valuable for a press manufacturer because machine accuracy depends on the relationship between individual components rather than on any single part alone.
Advanced precision-processing equipment supports the production of components requiring controlled dimensions and consistent interfaces. Machining quality is especially relevant to slide guides, table surfaces, mounting areas, shafts, gears, connecting components, and other parts that influence alignment and motion. Consistency during machining can reduce adjustment requirements during assembly and improve repeatability between machines.
The company also emphasizes non-standard customization. Battery manufacturers often require special worktable layouts, feeding systems, die interfaces, automation connections, safety configurations, electrical standards, or process-specific modifications. A manufacturer with in-house engineering and customization capability may be better positioned to adapt the press to an individual production line than a supplier offering only a fixed standard configuration.
Press quality is established through many stages rather than a single final test. Material selection, casting or steel fabrication, machining, heat treatment where required, component inspection, subassembly, alignment, electrical testing, lubrication verification, and load testing all contribute to the final machine condition.
The manufacturer describes a finished-product inspection system intended to exceed ordinary industry requirements. In practical terms, a robust inspection program should verify frame geometry, table flatness, slide parallelism, die-height adjustment, drive operation, lubrication delivery, motor performance, control functions, emergency stopping, guarding, and operating noise or vibration.
For a battery-component press, dimensional accuracy and repeatability should be assessed under conditions that reflect actual operation. A no-load test alone cannot reveal every issue that may appear during forming. Where feasible, customer-specific tooling trials or representative load tests can help confirm that the machine and process are compatible before shipment or final acceptance.
Traceable inspection records are valuable for future maintenance and quality audits. They provide a baseline against which the machine can be evaluated during service. For international customers, documentation should also cover electrical configuration, spare parts, lubrication recommendations, installation requirements, safety instructions, and operating procedures.
Successful installation begins before the machine arrives. The purchaser should confirm the foundation design, transportation route, lifting capacity, floor loading, electrical supply, compressed-air availability, ventilation, lighting, working clearance, and material-handling arrangement. The BLPC II-80 requires an air pressure supply of approximately 0.55 MPa for its specified pneumatic functions, subject to the final machine configuration.
The foundation must be capable of supporting the machine and resisting operating vibration. Leveling should be completed with suitable instruments, and the machine should be anchored according to the manufacturer’s instructions. Incorrect leveling can influence slide movement, die alignment, lubrication distribution, and long-term frame loading.
Commissioning should include mechanical inspection, electrical connection verification, lubrication-system testing, drive-system testing, inching and single-cycle operation, emergency-stop testing, and confirmation of safety devices. The machine should not be placed into automatic production until all protective systems and operating controls have been verified.
Die installation requires equal care. The die must be compatible with the table and slide dimensions, weight limits, shut height, force requirements, and mounting arrangement. The die should be centered and secured correctly, with adequate clearance for feeding and part removal. Trial cycles should begin at a conservative speed before the production rate is increased.
Preventive maintenance helps preserve accuracy, reliability, and productivity. Operators should perform routine checks of lubricant level, lubrication alarms, air pressure, unusual noise, vibration, fasteners, guards, electrical indicators, and visible wear. Any abnormal condition should be investigated before it develops into a major failure.
Scheduled maintenance should include inspection of slide guides, connecting components, drive elements, bearings, shafts, fasteners, pneumatic equipment, electrical cabinets, sensors, and die-height adjustment mechanisms. The intervals should be adjusted according to operating hours, production speed, environment, material contamination, and load severity.
Automatic lubrication simplifies regular operation but does not replace cleaning and inspection. Lubricant lines should be checked for blockage or leakage, and reservoirs should be replenished with the correct material. Contaminants around the die area should be removed so that they do not enter moving components or interfere with sensors and guide surfaces.
Service support is another important part of machine ownership. The manufacturer describes a customer-oriented system covering pre-sales consultation, in-sales support, and after-sales service. For international users, response time, spare-parts availability, remote troubleshooting, technical documentation, and local service arrangements should be confirmed during procurement.
The BLPC2-80 should be selected after reviewing the complete production process rather than relying only on the nominal force. Important questions include:
What material will be formed, and what are its thickness, tensile strength, yield strength, and work-hardening characteristics?
What is the maximum required forming force, and where does the peak force occur in the stroke?
What are the die’s overall dimensions, closed height, weight, and center of load?
Does the component require deep drawing, progressive stamping, trimming, piercing, embossing, or multiple operations?
What production speed is required, and can the feeding and unloading systems operate reliably at that speed?
What level of dimensional accuracy, flatness, surface quality, and repeatability is required?
Will the machine be integrated with a decoiler, straightener, feeder, transfer system, robot, vision inspection system, or other automation?
Answering these questions enables the manufacturer and customer to confirm the proper configuration, tooling, controls, safety equipment, and auxiliary systems. It also helps prevent the common mistake of selecting a press solely according to its largest advertised capacity.
Manufacturers competing in the battery supply chain must control quality, cost, delivery time, and production flexibility simultaneously. A specialized press can contribute to competitiveness when it reduces setup limitations, supports stable high-volume operation, and accommodates new components without major equipment changes.
The BLPC2-80 offers a useful combination of features for this purpose. Its 800 kN capacity provides meaningful forming force. Its 180 mm stroke supports deeper components. Its double-point structure is appropriate for wider dies and more evenly distributed loading. Its large worktable and 320 mm die-height capability improve tooling flexibility. Its rigid steel frame supports stable forming, while electric automatic lubrication helps maintain the machine during repeated production.
Compared with purchasing several smaller presses for different operations, one appropriately selected double-point press may simplify production planning and reduce the number of machine interfaces. Compared with choosing a much larger press than necessary, the 800 kN class may offer a more balanced relationship between capability, space, energy use, and capital investment. The final economic result depends on utilization, tooling, labor, automation, maintenance, and product volume, but the machine’s specification provides a strong basis for efficient operation.
The BLPC2-80 is an open-type double-point mechanical power press designed for high-precision metal forming. It is especially suited to battery housings, covers, trays, structural components, and related stamped parts.
The nominal capacity is 800 kN. The actual suitability for a particular operation must be confirmed through force calculations that consider material, thickness, tooling, forming method, and the location of peak force.
A double-point design introduces force through two connection points, helping distribute load across a wider slide. This can improve stability for broad dies, reduce the tendency toward slide tilting, and support more consistent forming across the work area.
The slide stroke is 180 mm. This extended travel provides additional flexibility for deeper battery housings and forming operations requiring greater vertical movement.
The worktable measures 1600 × 610 × 130 mm. The large mounting area can accommodate broad dies, progressive tooling, and auxiliary equipment when the total load remains within the machine’s limits.
The maximum die height is 320 mm, with an adjustment range of 80 mm. The final die compatibility should be checked against the specific die’s closed height, weight, mounting arrangement, and operating requirements.
The rated speed range is approximately 45–75 strokes per minute. The correct production speed depends on material flow, die design, lubrication, feeding, part removal, quality requirements, and safety conditions.
Yes. The machine includes an electric automatic lubrication system intended to provide scheduled lubrication to relevant moving components. Operators must still inspect the lubricant level, lines, pump, alarms, and component condition.
Yes. The press can be applied to various metal stamping and forming operations, including structural parts, covers, trays, brackets, plates, and other components. Compatibility depends on the material, tooling, force requirement, dimensions, and process sequence.
The manufacturer provides non-standard design and manufacturing services. Possible customization areas may include tooling interfaces, automation integration, electrical standards, feeding arrangements, safety systems, and special process requirements. Each project should be reviewed technically before confirmation.
The listed power supply is three-phase 380 V at 50 Hz. Customers should verify local electrical requirements and confirm the final configuration before ordering and installation.
Customers should provide the material specifications, part drawings, forming process, die dimensions, required capacity, production speed, automation plan, plant conditions, electrical standards, and safety requirements. These details allow the machine and tooling package to be evaluated as a complete system.
The BLPC2-80 Multi-Spec High-Precision Open-Type Double-Point Battery Power Press is engineered for manufacturers seeking a capable and flexible forming platform for battery-related metal components. Its 800 kN nominal capacity, 180 mm slide stroke, 1600 × 610 mm worktable, 320 mm maximum die height, and 80 mm die-height adjustment provide a substantial working envelope for medium-to-large tooling.
The double-point structure and high-rigidity steel frame support stable load distribution and accurate forming, while the electric automatic lubrication system contributes to dependable operation and planned maintenance. The 45–75 strokes-per-minute range allows users to balance productivity with process stability according to the requirements of each component.
Beyond the machine specifications, the manufacturer’s integrated approach to research, design, precision processing, assembly, inspection, customization, and service is an important part of the product’s value. For battery manufacturers, this combination can support more reliable equipment selection, smoother integration, and stronger long-term production performance.
As with any industrial press, final suitability must be confirmed through engineering analysis, force calculation, tooling review, safety evaluation, installation planning, and production trials. When properly selected and maintained, the BLPC2-80 can serve as a durable and adaptable foundation for precise battery housing production and other demanding metal-forming applications.
1. Manufacturer-provided technical data for the BLPC II open-type double-point battery power press series.
2. Manufacturer-provided product description for the BLPC2-80 multi-spec high-precision open-type double-point battery power press.
3. Manufacturer-provided company information concerning research and development, manufacturing, quality control, customization, and service capabilities.
4. General principles of mechanical power press selection, die design, forming-force calculation, and preventive maintenance.
5. General industrial guidance on metal forming for battery housings, energy-storage enclosures, and stamped structural components.


A buyer comparing a 45-ton open-gap press for a bracket line often receives two...
What Is a Power Press? A power press — also called a stamping press or punch pr...
Understanding Mechanical Power Presses and Their Essential Functions A mechani...
In the fields of metal forming, sheet metal fabrication, blanking, and punching,...
Two presses can both carry a 200-tonne nameplate and still produce very differe...
Start With the Purchase Decision, Not the Definitions A procurement engineer co...
Contact Us

topbolun@gmail.com

+86-575-83362228

+86-13735238388
+86-18667502750

+86-575-83362999

+8618667502750

No.1 Linjiang Road East, Xiaren, Jinting Town, Shengzhou City, Zhejiang Province, China
Ready to Begin?
Get in Touch

Now!

ZHEJIANG BOLUN
 English
 中文简体