Modern metal-forming operations demand more than nominal tonnage. A production press must deliver stable force, maintain precision over long operating cycles, accommodate demanding dies, protect operators and tooling, and integrate smoothly into a manufacturing line. The BLPD-260 Industrial Strength Deep-Stroke Semi-Closed Single-Point Power Press is designed for these requirements. With a nominal capacity of 2,600 kN, a 250 mm slide stroke, a maximum die height of 550 mm, and a 32-ton machine structure, it is positioned for deep forming, heavy-duty forging, and large-scale industrial stamping.
The machine combines a semi-closed single-point frame with a high-rigidity construction, a 22 kW main motor, automatic lubrication, hydraulic overload protection, tonnage monitoring, and dual solenoid valve stopping control. These features are not isolated specifications. Together, they create a forming system capable of maintaining dependable force transmission and controlled movement when production conditions become demanding.
For manufacturers comparing conventional power presses, the BLPD-260 offers a practical balance between capacity, working depth, die compatibility, operating stability, and serviceability. Its configuration is especially suitable for customers who need more forming space and deeper slide movement than a standard shallow-stroke stamping press can provide, without moving entirely to a more complex and slower hydraulic forming system.
This article examines the machine’s technical characteristics, operating advantages, competitive value, manufacturing quality, safety functions, application range, maintenance requirements, and the capabilities of the company that designs and produces it.
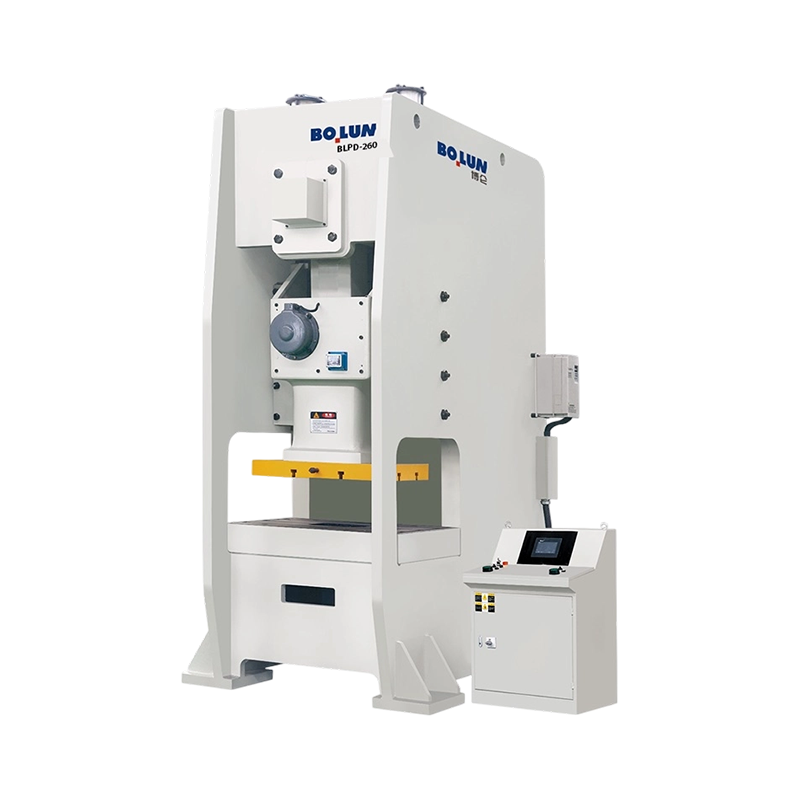
BLPD-260 Industrial Strength Deep-Stroke Semi-Closed Single-Point Power Press
The BLPD-260 belongs to the semi-closed single-point power press category. This configuration is widely used where a robust frame, a single central drive point, and reliable mechanical motion are required for repetitive stamping and forming work. The semi-closed design provides a useful compromise between open accessibility and structural stiffness. Operators and production engineers can benefit from convenient die access while retaining a reinforced load-bearing structure suitable for high-capacity applications.
The machine has a nominal capacity of 2,600 kN. In practical terms, this capacity gives manufacturers the force reserve required for demanding operations such as deep drawing, large-part forming, heavy blanking, bending, coining, and industrial component production. Nominal capacity alone does not determine whether a press is appropriate for a particular job. The position of the nominal pressure point, the selected stroke, die geometry, material properties, lubrication conditions, and production speed must also be considered. However, a 2,600 kN rating provides a substantial working platform for large and difficult-to-form components.
The 250 mm slide stroke is one of the machine’s most important advantages. A deeper stroke provides additional vertical travel for dies that require extended forming movement, multi-stage operations, or greater clearance during loading and unloading. Compared with presses designed primarily for short-stroke high-speed work, the BLPD-260 is better suited to applications where the workpiece must travel farther through the forming cycle.
The maximum die height is 550 mm, with a die-height adjustment range of 120 mm. This allows the press to accept large tooling assemblies and provides flexibility when different dies are used in the same production area. Die compatibility is a major cost factor in industrial stamping. A machine that can accept a broader range of tooling reduces the need for extensive die modification and helps manufacturers serve more product variations.
The worktable measures 1,140 by 840 mm, while the slide bottom measures 1,130 by 650 mm. These dimensions create a substantial working envelope for medium-to-large dies. The 1,020 mm working-face height also supports practical material handling and integration with auxiliary equipment. The distance between columns is 1,230 mm, offering useful lateral access and sufficient space for large workpieces and tooling arrangements.
| Specification | BLPD-260 Value |
|---|---|
| Machine category | Semi-closed single-point power press |
| Nominal capacity | 2,600 kN |
| Slide stroke | 250 mm |
| Strokes per minute | 20–40 S.P.M. for the listed vertical configuration |
| Maximum die height | 550 mm |
| Die-height adjustment | 120 mm |
| Worktable size | 1,140 × 840 × 180 mm |
| Slide bottom size | 1,130 × 650 × 100 mm |
| Working-face height | 1,020 mm |
| Distance between columns | 1,230 mm |
| Main motor | 22 kW × 4-pole configuration |
| Press weight | 32 tons |
| Air pressure | 0.55 MPa |
| Mold pad capacity | 140 kN |
| Ram stroke | 100 mm |
| Effective cushion area | 810 × 480 mm |
| Punch accuracy classification | GB/JIS Class 1 |
Deep forming requires coordinated control of stroke length, force, die space, material flow, and tooling support. A press with insufficient stroke may force manufacturers to redesign the die, reduce part depth, add extra operations, or accept poor material distribution. The 250 mm slide stroke of the BLPD-260 is intended to address this challenge directly.
In deep drawing and related forming processes, the blank is progressively moved into a die cavity while the material is guided and controlled by the punch, die, and hold-down system. The available stroke must be sufficient to complete the forming movement while allowing adequate clearance for the workpiece, die components, and part removal. A longer stroke also gives production engineers greater flexibility when designing forming sequences and selecting blank-holder arrangements.
The BLPD-260 includes a mold pad capacity of 140 kN and a 100 mm ram stroke. This support system can assist forming operations that require controlled counterforce, bottom support, or workpiece ejection. The effective cushion area is 810 by 480 mm, giving the machine a broad support surface for large dies. These capabilities are valuable when forming quality depends on controlled material movement rather than on simple downward pressing alone.
The machine is not limited to one type of forming operation. Its deep-stroke architecture can support large-scale stamping, heavy blanking, bending, embossing, coining, and selected forging processes, provided that the die design and process parameters are correctly matched to the machine’s capacity. The same press can therefore support multiple production programs, improving equipment utilization and reducing the number of specialized machines required in a facility.
Large dies often create challenges that are not present in compact stamping applications. They may require greater installation height, larger worktable dimensions, higher closing force, more robust slide support, and increased structural resistance to deflection. The BLPD-260 addresses these demands through its 550 mm maximum die height, 1,140 by 840 mm worktable, and heavy 32-ton structure.
A large working area reduces the risk of overhanging tooling and makes it easier to distribute the load across the table. It also provides space for progressive, compound, transfer, or multi-stage die components. While the final suitability of a die must always be checked by engineering personnel, the BLPD-260’s dimensions provide a strong foundation for large-format production.
The semi-closed frame contributes to accessibility during die installation and setup. At the same time, the frame is designed to retain rigidity under high loading. This balance is important because a press that is easy to access but insufficiently stiff may suffer from alignment problems, accelerated wear, or inconsistent part quality. Conversely, a highly enclosed configuration may complicate setup and maintenance. The semi-closed design offers a practical compromise for factories that need both production strength and reasonable working access.
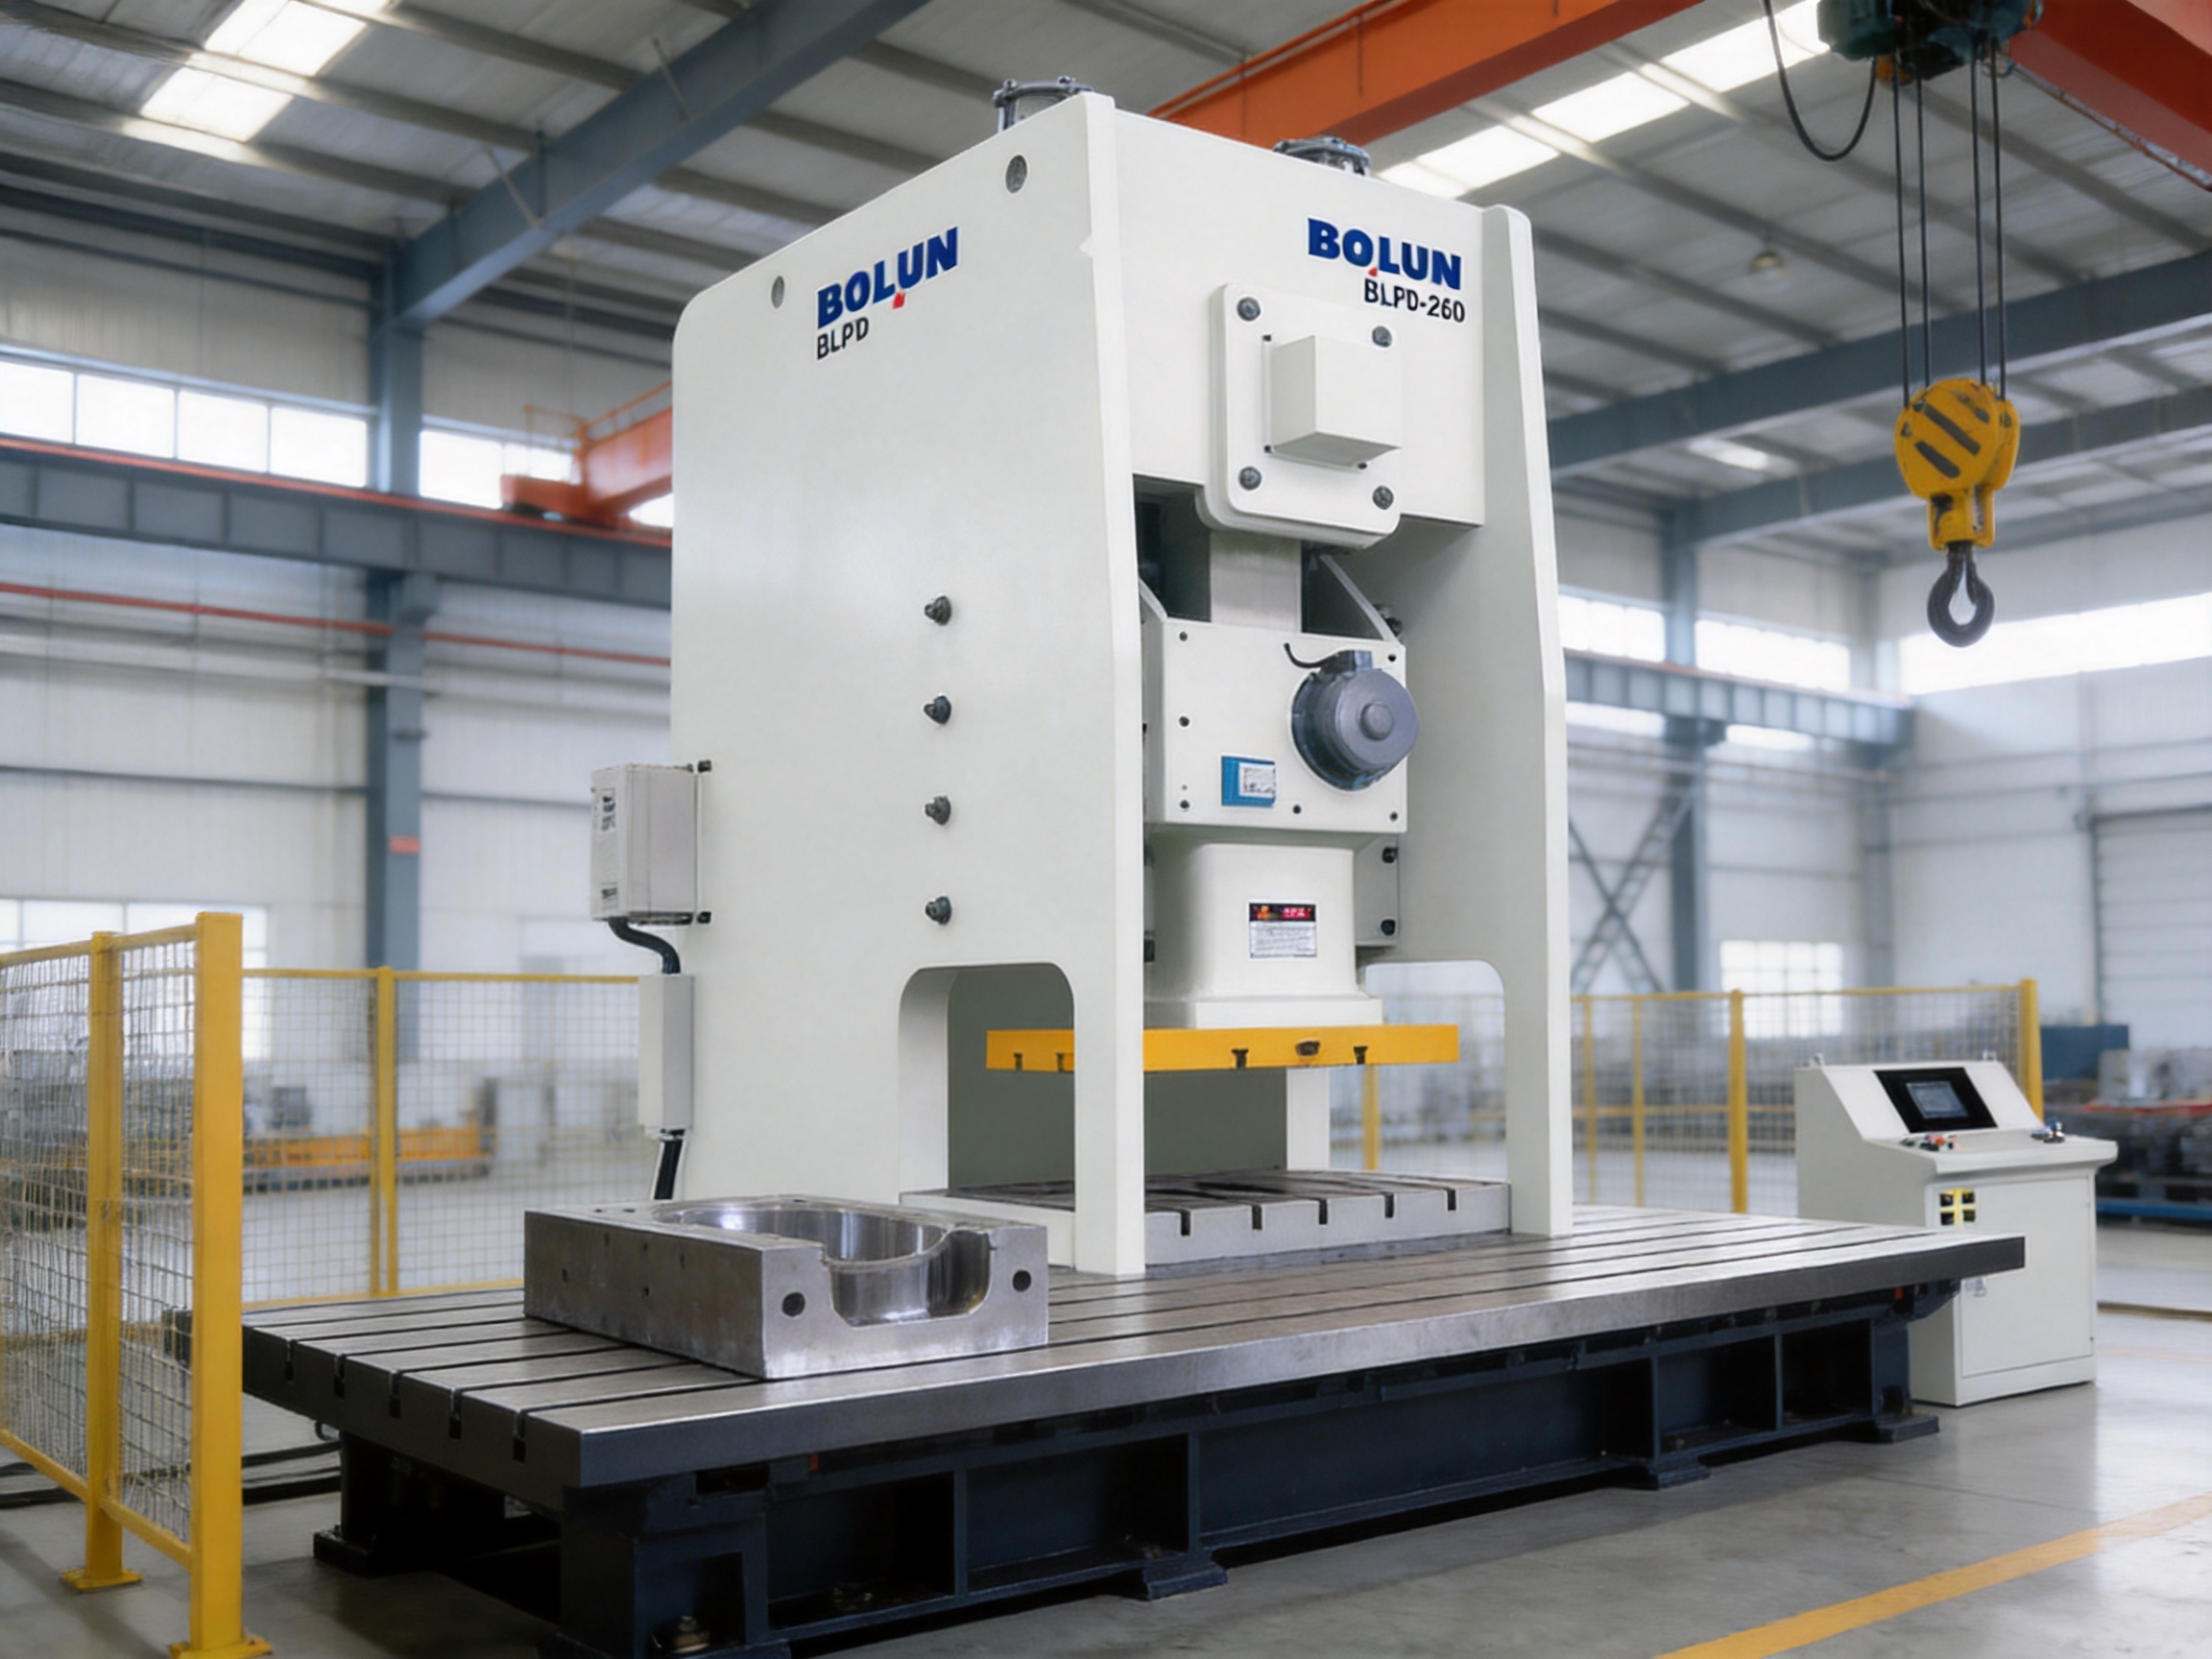
Press-frame rigidity is one of the clearest distinctions between a basic machine and an industrial-grade machine. When a press applies high forming force, the frame, slide, table, columns, crank mechanism, and die all experience loads. Elastic deformation is unavoidable to some extent, but excessive or uneven deformation can affect dimensional accuracy, increase die wear, and create uneven contact conditions.
The BLPD-260 is constructed as a high-rigidity 32-ton machine. The weight of the structure is significant because it reflects the mass required to resist vibration and absorb dynamic forces. A heavier, properly engineered frame can reduce movement during the working stroke and help maintain more stable alignment between the slide and the table.
Structural stability is especially important during continuous high-load production. A machine used occasionally for light work may tolerate a less substantial frame, but a press used throughout multiple shifts must maintain performance while exposed to repeated acceleration, deceleration, impact, and forming loads. The BLPD-260 is positioned for this type of demanding service.
High rigidity also benefits tooling life. When the slide and table remain more stable, the die is less likely to experience uneven loading. This can reduce localized wear on punches, die blocks, guide components, and cutting edges. Tooling is often one of the most expensive assets in a stamping operation, so protecting it can produce significant long-term savings.
Vibration affects more than operator comfort. It can influence noise, surface quality, dimensional repeatability, fastener loosening, electrical reliability, and the service life of moving components. The 32-ton machine structure and rigid frame help provide a stable base for the press mechanism. When combined with correct foundation preparation and installation, this can support smoother operation and more consistent production.
Repeatability is particularly valuable when a press is used with automated feeding, transfer devices, sensors, or inspection systems. These systems depend on predictable slide motion and stable die alignment. If the press experiences excessive movement, the material may not enter the die consistently, and sensors may detect variable conditions. A rigid platform improves the foundation for automation and process monitoring.
Manufacturers should still evaluate foundation requirements, anchoring, leveling, and surrounding equipment layout during installation. Even the strongest machine cannot perform correctly if it is installed on an unsuitable foundation or operated with improperly aligned tooling. The press’s structural advantages reach their full value when supported by disciplined installation and setup procedures.
The BLPD-260 uses a 22 kW main motor in a four-pole configuration. This motor is selected to provide the torque required for high-capacity forming work. A high-torque drive is important because the press must overcome the resistance created by the material and die during the working portion of each cycle. Adequate motor capacity also supports stable operation when the machine is used for demanding loads within its specified range.
The listed stroke rate for the BLPD-260 vertical configuration is 20 to 40 strokes per minute. This range reflects the machine’s deep-stroke, high-capacity positioning. It is not designed solely to maximize empty-cycle speed. Instead, it prioritizes force, travel, die compatibility, and stable forming performance. For many large industrial components, this operating range is appropriate because the forming process itself, rather than the press’s maximum cycle speed, determines production time.
Controlled mechanical motion helps reduce shock during the cycle. Smooth acceleration toward the working zone and stable movement through the forming area support better material flow and reduce unnecessary stress on the machine. The correct speed must always be determined according to the die, material, lubrication, part geometry, and required accuracy. A slower, controlled cycle can often provide better results than an aggressive cycle that increases wrinkling, tearing, vibration, or die wear.
The single-point drive arrangement applies force through a central connection. This configuration can support balanced movement when the die is correctly designed and the load is distributed properly. It is particularly suitable for applications where a central pressing action is preferred and where the workpiece is positioned within the machine’s effective working envelope.
The dual solenoid valve structure is designed to improve stopping control during operation. Redundant or coordinated valve arrangements can contribute to more dependable control of the clutch-brake or related pneumatic operating circuit, depending on the machine’s final configuration and applicable safety system. Precise stopping is essential during setup, inspection, fault response, and normal production.
Stopping performance must be considered together with control logic, guarding, emergency-stop circuits, operator procedures, and applicable machine safety standards. The dual solenoid arrangement provides an important hardware element, but safe operation depends on the complete system. Correct adjustment and regular testing are necessary to ensure that the stopping system continues to respond as intended.
Reliable stopping also supports die protection. If an abnormal condition occurs, a prompt and controlled stop can help prevent additional damage to the tooling or workpiece. This is especially important in high-capacity presses, where even a short continuation of movement may have significant consequences.
Overload protection is a central requirement for a press rated at 2,600 kN. Overloading may occur because of an incorrect die setting, excessive material thickness, misfed stock, foreign material, poor lubrication, or a process condition that exceeds the intended forming load. Without suitable protection, overload can damage the slide, crankshaft, connecting components, die, or frame.
The BLPD-260 incorporates hydraulic overload protection to help safeguard the press and tooling. When the applied load reaches an abnormal level, the protection system is intended to reduce the risk of severe mechanical damage. This contributes to lower downtime and can help prevent a relatively small setup error from becoming a costly repair event.
Hydraulic overload protection is most effective when it is correctly adjusted and maintained. Operators should not treat it as permission to operate beyond the machine’s rated limits. The protection system is a safeguard, not a substitute for correct die engineering, material verification, process calculation, and operator training. Loads should remain within the manufacturer’s recommended operating envelope.
The integrated tonnage monitoring display provides process visibility. Instead of relying only on sound, vibration, or visual inspection, production personnel can observe load information during the press cycle. This can help identify changes in material thickness, die condition, lubrication, alignment, or feeding accuracy.
Consistent tonnage is often an indicator of consistent process conditions. If the load pattern changes gradually, it may signal die wear or changes in material properties. If the load rises suddenly, it may indicate a misfeed, a blocked die, a double sheet, or an alignment problem. Early detection gives the operator an opportunity to stop the machine and investigate before the problem causes extensive damage.
Tonnage monitoring can also support preventive maintenance. Production teams can compare normal load patterns with later cycles and use the information to determine when inspection is appropriate. Over time, this creates a more data-informed maintenance approach. Instead of waiting for a failure, the factory can respond to measurable changes in operating behavior.
For quality management, load monitoring can contribute to process documentation. When a particular part requires a stable forming load, recorded observations can help verify that production remains within an acceptable range. The monitoring function does not replace dimensional inspection or material testing, but it adds another useful layer of process control.
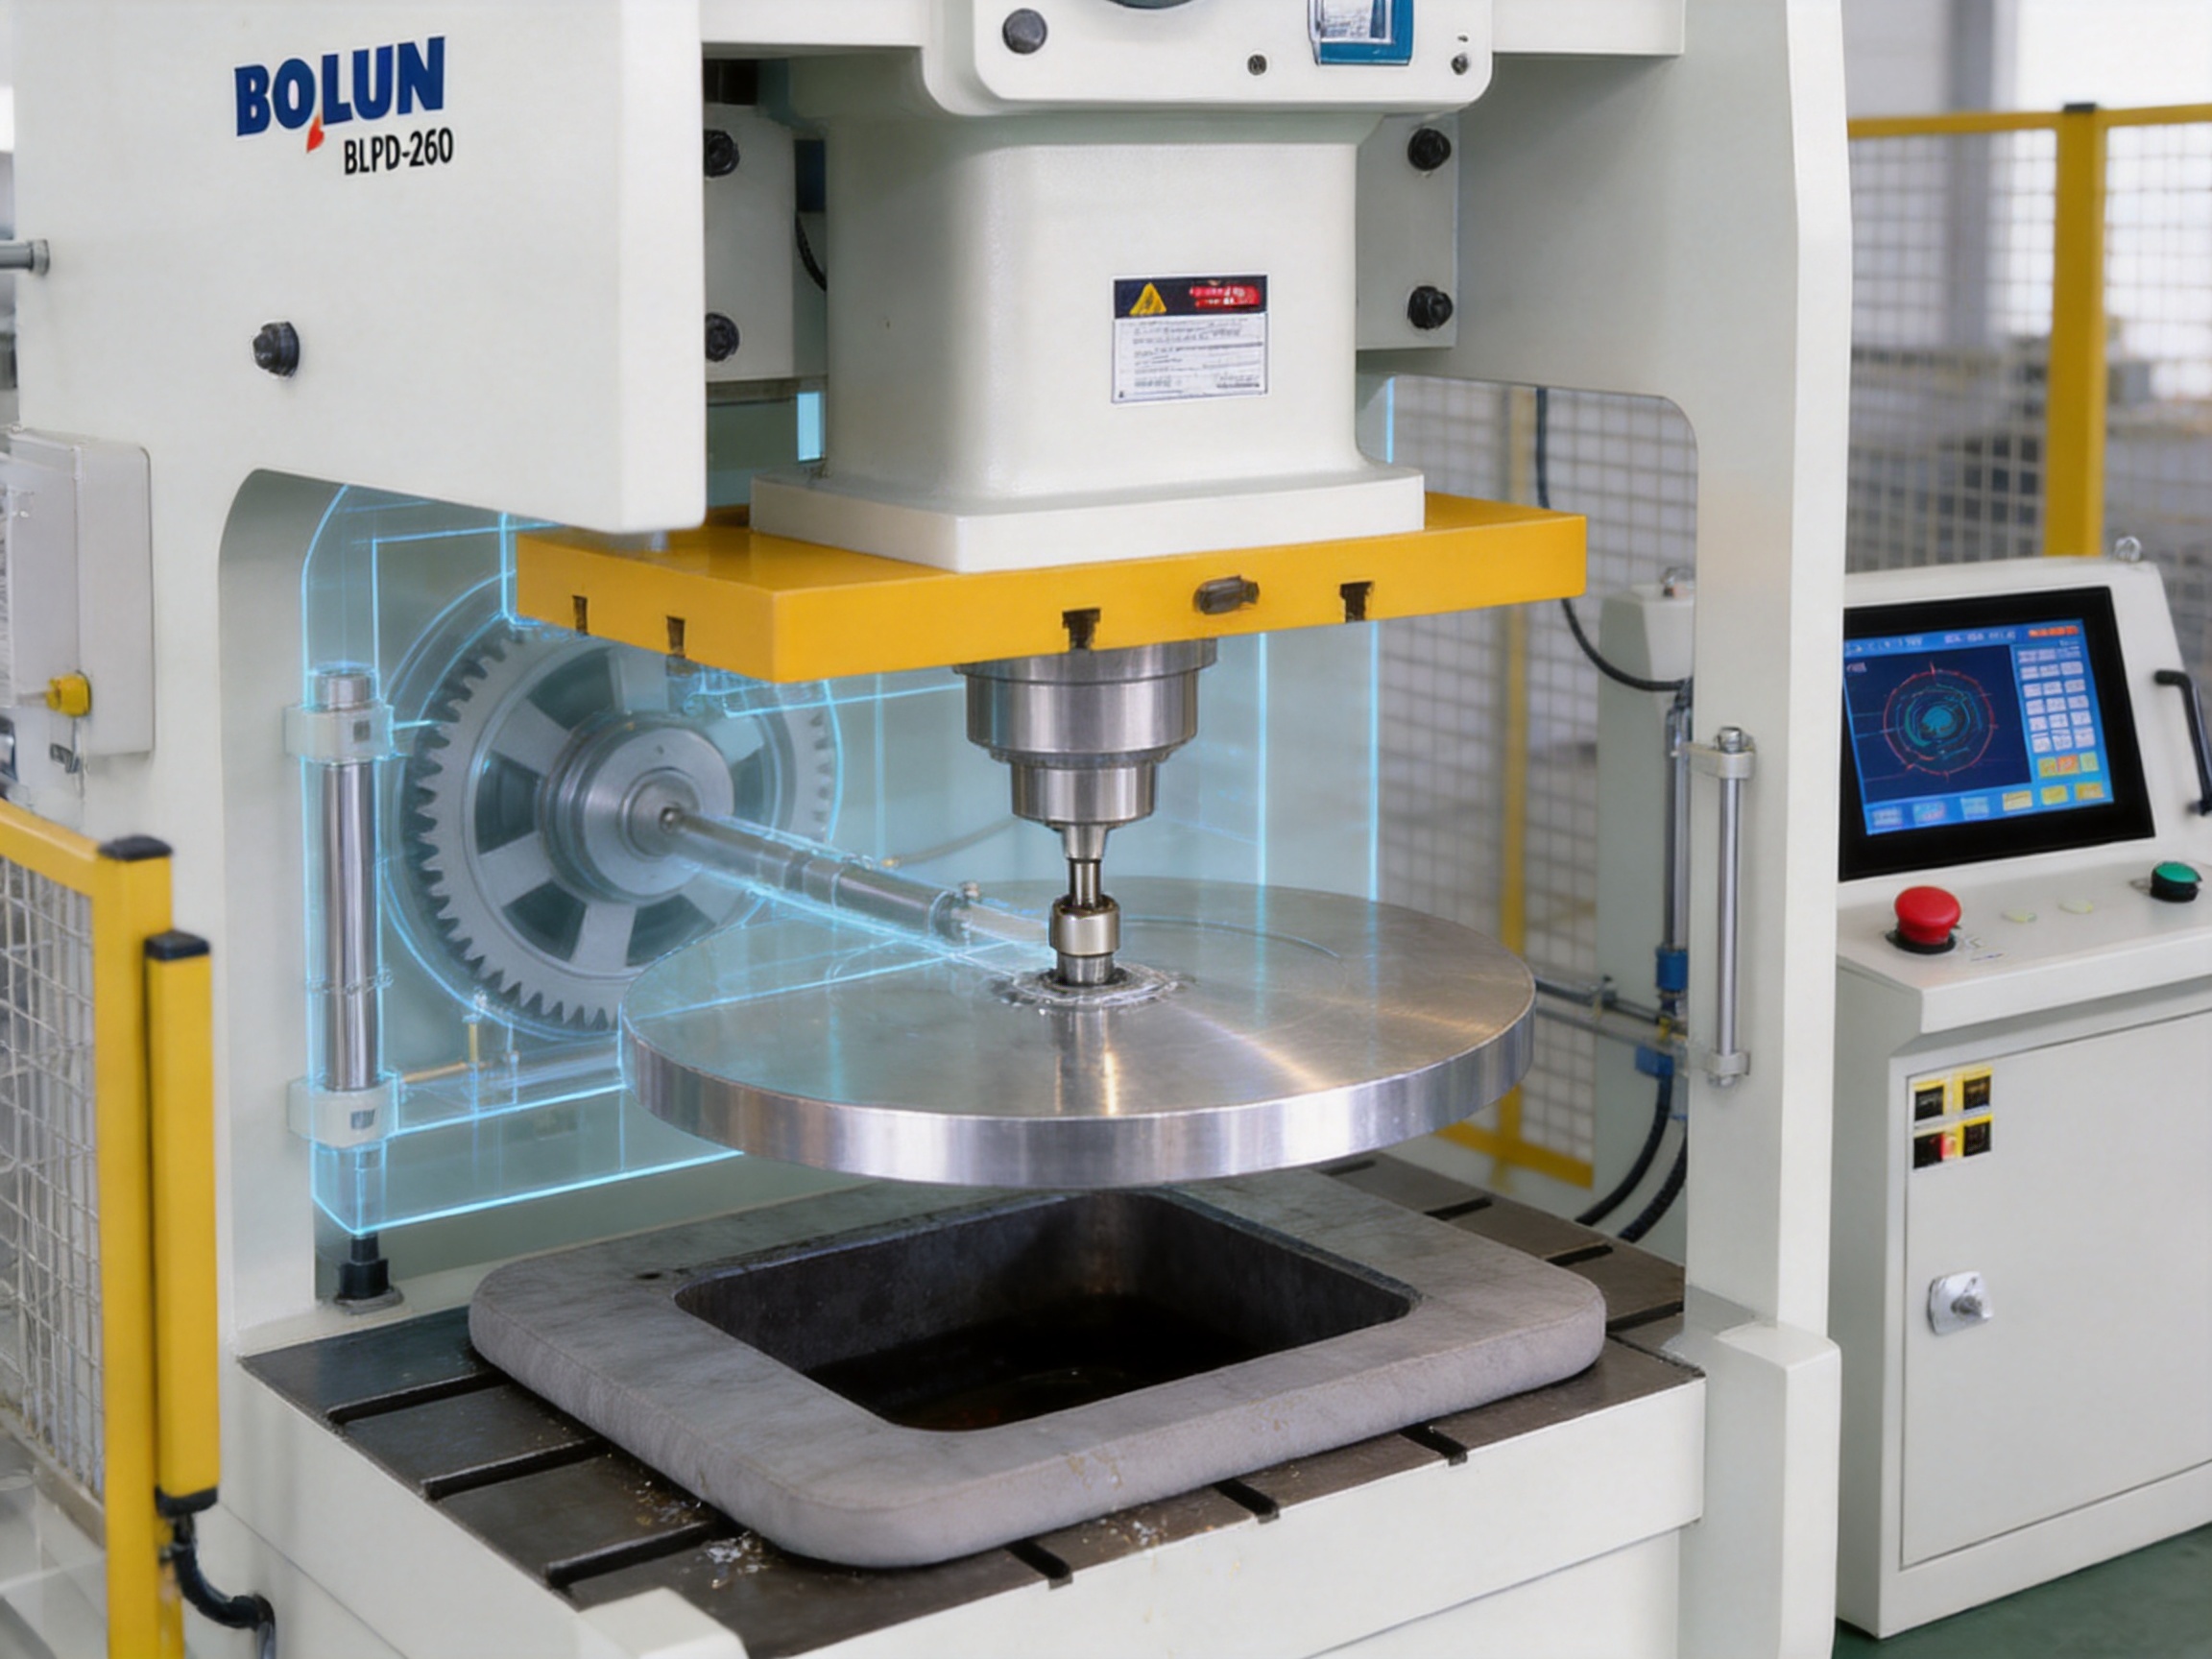
Lubrication affects nearly every mechanical system in a power press. Bearings, gears, guide surfaces, crank mechanisms, slide connections, and other moving parts require suitable lubrication to reduce friction and manage heat. In a high-load machine, insufficient lubrication can accelerate wear and create excessive temperature, noise, or vibration.
The BLPD-260 includes automatic lubrication to support consistent delivery of lubricant to designated components. Automatic systems reduce dependence on manual application and help ensure that lubrication occurs according to the machine’s operating requirements. This is especially beneficial in multi-shift production, where manual lubrication can be overlooked during busy periods.
Automatic lubrication also improves maintenance discipline. A system that is integrated into the machine can be checked, replenished, and monitored as part of a defined maintenance schedule. Operators can focus on production while maintenance personnel verify oil or grease levels, distribution lines, filters, and alarms.
It is important to use the correct lubricant and to follow the recommended service intervals. Automatic lubrication does not eliminate the need for inspection. Blocked lines, damaged fittings, contaminated lubricant, low reservoir levels, and pump problems must still be detected and corrected. Regular checks protect the benefits of the system.
The BLPD-260 is designed for substantial tooling. Its maximum die height of 550 mm provides vertical space for large dies and complex assemblies. The 120 mm die-height adjustment range allows the working position to be fine-tuned for different tool heights and process requirements.
Correct die-height adjustment is critical for protecting the press. The die must be installed at an appropriate height, the slide must be set correctly, and the shut height must be verified before production. Proper adjustment helps distribute load correctly and reduces the risk of bottoming, excessive clearance, incomplete forming, or damage to the die.
The worktable thickness of 180 mm contributes to a stable die-support surface. A substantial table can help resist local deformation and maintain the relationship between the lower die and the press frame. The table dimensions of 1,140 by 840 mm are suitable for large industrial tooling while still allowing practical access around the machine.
The slide bottom measures 1,130 by 650 by 100 mm. This provides a broad mounting area for the upper die and supports the installation of tooling with significant lateral dimensions. Engineers should verify mounting-hole patterns, T-slots, die weight, center of gravity, and lifting requirements before installation.
The 1,230 mm distance between columns is another practical advantage. It allows larger workpieces to pass through the working area and improves access during setup. In production environments, good access can shorten die-change times and make inspection tasks easier. It can also support the integration of feeders, blank loaders, conveyors, and part-removal devices.
The 140 kN mold pad capacity and 100 mm ram stroke expand the press’s process range. A cushion or pad may be used to control material flow, provide counterpressure, assist in drawing, or eject the formed component. Its effectiveness depends on the specific die arrangement and process design, but the available capacity is significant for a machine of this class.
The effective cushion area of 810 by 480 mm provides broad support beneath the die. This is useful for large parts where localized support could create uneven forming or excessive stress. A well-designed cushion system can improve bottom conditions, reduce wrinkles, assist part release, and support more consistent forming results.
Tool designers should calculate cushion force, pressure distribution, stroke requirements, and timing carefully. Excessive cushion force may restrict material flow and cause tearing, while insufficient force may result in wrinkling or poor shape control. The press provides the mechanical capability, but successful results depend on matching the machine to the die and material.
The listed punch accuracy classification is GB/JIS Class 1. This indicates that the machine is designed for a high level of punching accuracy within the applicable standard framework. Accuracy in a power press is influenced by frame rigidity, slide guidance, die alignment, manufacturing tolerances, lubrication, foundation quality, and maintenance condition.
Precision is not simply a measurement taken once during factory acceptance. It is a continuing production objective. A machine may leave the factory within specification, but its long-term accuracy depends on correct installation, suitable tooling, regular inspection, controlled loading, and timely replacement of worn components.
The BLPD-260’s rigid structure, controlled slide motion, load monitoring, and automatic lubrication work together to support repeatable production. When these features are combined with accurately manufactured dies and properly prepared materials, the press can help manufacturers achieve consistent dimensions and surface quality across long production runs.
For deep forming, repeatability is especially important. Small variations in slide position, blank-holder pressure, lubrication, or die alignment can create visible differences in wall thickness, surface finish, springback, and final dimensions. A stable press platform helps reduce one major source of variation and allows process engineers to focus on material and tooling optimization.
The company behind the machine, Zhejiang Bolun High-Precision Machinery Co., Ltd., is based in Zhejiang, China, a region known for its developed manufacturing infrastructure and strong machinery supply chain. The company has approximately two decades of experience in machinery manufacturing and has developed capabilities covering research and development, design, production, sales, and service.
Its manufacturing approach is based on an integrated production system rather than simple equipment assembly. This distinction matters for large presses because performance depends on the relationship between the frame, drive system, control components, lubrication circuit, overload protection, slide guidance, table, and die-adjustment mechanisms. When these elements are designed and managed within a coordinated system, the manufacturer can better control compatibility and quality.
The company maintains advanced precision-processing equipment and an industrial production environment that covers multiple stages of machine development. These stages include basic structural design, core component development, precision machining, assembly, testing, and final inspection. Such integration gives the producer greater control over critical dimensions and reduces dependence on loosely coordinated external processes.
Research and development is important because customers do not always require a standard machine configuration. Different industries may need special die heights, unusual working-table dimensions, customized feeding arrangements, additional monitoring, special electrical specifications, or modifications for a particular material and product shape.
The company provides non-standard customization and one-stop design and manufacturing services for products with special specifications and functions. This capability allows customers to discuss production requirements at the equipment-design stage rather than attempting to adapt an unsuitable standard machine after purchase.
Customization can involve more than changing dimensions. It may include process analysis, die-space evaluation, control-system requirements, auxiliary equipment interfaces, safety guarding, material flow, and factory layout. A manufacturer with design and production experience can help assess whether a proposed configuration is technically and economically appropriate.
Large power presses require accurate machining of load-bearing and moving components. The frame must maintain correct geometry, the table and slide must remain properly related, and guide systems must support stable movement. Precision processing helps control the dimensional relationships that determine machine performance.
Assembly quality is equally important. Even accurately machined parts can produce poor results if assembled without suitable alignment, measurement, adjustment, and testing. The producer’s integrated production model supports a controlled transition from machining to assembly and final commissioning.
For customers, this means the purchase decision is not based solely on a catalog number. It also includes confidence in the manufacturer’s ability to produce, inspect, adjust, and support the entire machine. This is particularly valuable for high-capacity equipment, where transportation, installation, commissioning, and service require coordinated technical planning.
Quality control is described as a core principle of the company’s manufacturing system. The company applies inspection procedures to finished products, components, and production processes. For a large power press, inspection should address structural dimensions, slide movement, die-height adjustment, lubrication performance, electrical functions, stopping performance, overload protection, tonnage monitoring, and overall operating behavior.
A rigorous inspection system reduces the risk that hidden manufacturing variation will reach the customer. It also creates a foundation for traceability and continuous improvement. When inspection data is collected across machines and production stages, the manufacturer can identify recurring issues and improve design, processing, or assembly methods.
The company’s emphasis on quality is connected to the intended service life of the equipment. Industrial customers generally evaluate a press by total ownership value rather than purchase price alone. A machine that maintains stable precision, protects dies, reduces unplanned downtime, and receives timely service may provide better value than a lower-cost machine with weaker long-term support.
Quality assurance should continue after delivery. The company provides a customer-oriented service system covering pre-sales consultation, in-sales support, and after-sales guarantees. This lifecycle approach is important because the customer’s actual results depend on installation, commissioning, operator instruction, preventive maintenance, and technical response throughout the equipment’s working life.
The BLPD-260 competes in a market that includes basic open-frame presses, short-stroke stamping machines, hydraulic presses, and other high-capacity mechanical presses. Each machine class has appropriate uses, but the BLPD-260 offers a distinctive combination of features for deep and heavy forming.
Basic open-frame presses can be attractive for light and medium stamping because they are compact, accessible, and often economical. However, a high-capacity deep-forming job may expose limitations in their frame stiffness, die space, stroke, and resistance to deflection. The BLPD-260 provides a much heavier structure, a longer 250 mm stroke, a larger die space, and a 2,600 kN nominal capacity.
For manufacturers producing larger parts or operating under sustained load, these characteristics can result in greater process stability and longer tooling life. The semi-closed construction also provides a more robust load path than many lighter open-frame configurations.
High-speed presses are effective when the product is small, the material feed is optimized, and the forming operation is relatively shallow. Their principal advantage is cycle speed. However, speed is not always the most important factor. A deep component may require a longer stroke and greater die height, and forcing such a job onto a short-stroke machine can increase the number of operations or reduce product quality.
The BLPD-260 operates at a listed 20 to 40 strokes per minute, but it provides a 250 mm stroke and a 550 mm maximum die height. This makes it better suited to forming depth and die flexibility than a machine optimized only for rapid short movements.
Hydraulic presses provide highly flexible force and stroke control and can be excellent for certain deep-drawing and forming processes. However, they may involve different cycle characteristics, energy behavior, maintenance requirements, and production economics. A mechanical power press such as the BLPD-260 can offer efficient repetitive motion and a practical choice for continuous industrial stamping where a defined mechanical cycle is desirable.
The best choice depends on the material, part geometry, required force curve, production volume, tolerance, and automation plan. The BLPD-260 is particularly attractive when the customer wants the productivity and repeatability of a mechanical press while still requiring deep-stroke capability and large die accommodation.
Using a press close to its maximum limit can reduce process margin and increase sensitivity to material variation. A 2,600 kN machine provides capacity reserve for demanding jobs within its design range. This reserve can help manufacturers accommodate changes in material thickness, product design, tooling requirements, and future production programs.
Capacity reserve should not be confused with permission to overload the machine. The correct approach is to select a press that can complete the process comfortably and safely while observing rated loads, pressure points, die limits, and operating instructions.
The BLPD-260 is suitable for a broad range of industrial metal-forming applications. Its exact use depends on tooling and process engineering, but potential applications include automotive components, agricultural machinery parts, construction equipment components, electrical enclosures, industrial hardware, appliance parts, metal containers, structural brackets, and forged or stamped components requiring substantial force.
Deep forming is a central application. The 250 mm stroke and large die space support workpieces that cannot be produced efficiently on a shallow-stroke machine. The cushion system can assist material control, while the rigid structure helps maintain alignment during the forming cycle.
Heavy-duty blanking is another potential application. Large blanks and thick materials require high cutting force and a stable die-support platform. The 2,600 kN capacity and hydraulic overload protection provide an appropriate foundation for such work, subject to engineering verification of the actual cutting load and die design.
Bending, embossing, coining, and shaping operations can also benefit from the machine’s force and working area. For complex components, a single press may perform multiple operations using interchangeable dies. This can improve equipment utilization and help manufacturers respond to changing production schedules.
Forging-related applications require especially careful evaluation because forging loads can be highly dynamic and may differ from ordinary stamping loads. Customers should confirm material, temperature, die type, impact characteristics, cycle requirements, and load distribution with the manufacturer before selecting the machine for a specific forging process.
A machine of this size requires thorough preparation before delivery. The overall dimensions are approximately 2,180 by 2,850 by 4,470 mm, and the press weight is approximately 32 tons. The factory floor, foundation, transportation route, lifting equipment, electrical supply, compressed-air system, and maintenance access must all be planned in advance.
Foundation preparation should consider the machine’s static weight and dynamic operating forces. The installation area must be level and capable of supporting the press and associated tooling. Anchoring and leveling should be completed according to the manufacturer’s technical documentation. Poor leveling can affect slide guidance, die alignment, lubrication distribution, and long-term structural behavior.
Electrical installation must match the machine’s rated requirements and local regulations. The 22 kW main motor is only one part of the total electrical demand. Auxiliary motors, controls, lubrication equipment, safety circuits, and die-height adjustment systems should be included in the power calculation.
The machine uses an air pressure specification of 0.55 MPa. The factory compressed-air system should provide clean, dry, and stable air at the required pressure and flow. Air quality is important for solenoid valves, stopping functions, and pneumatic control components. Filters, regulators, drains, and maintenance procedures should be provided as part of the installation.
Commissioning should include inspection of the frame, table, slide, die-height mechanism, lubrication circuit, overload system, tonnage display, stopping controls, emergency devices, and operating modes. Trial cycles should begin at low speed and without production material, followed by controlled testing with the intended die and workpiece.
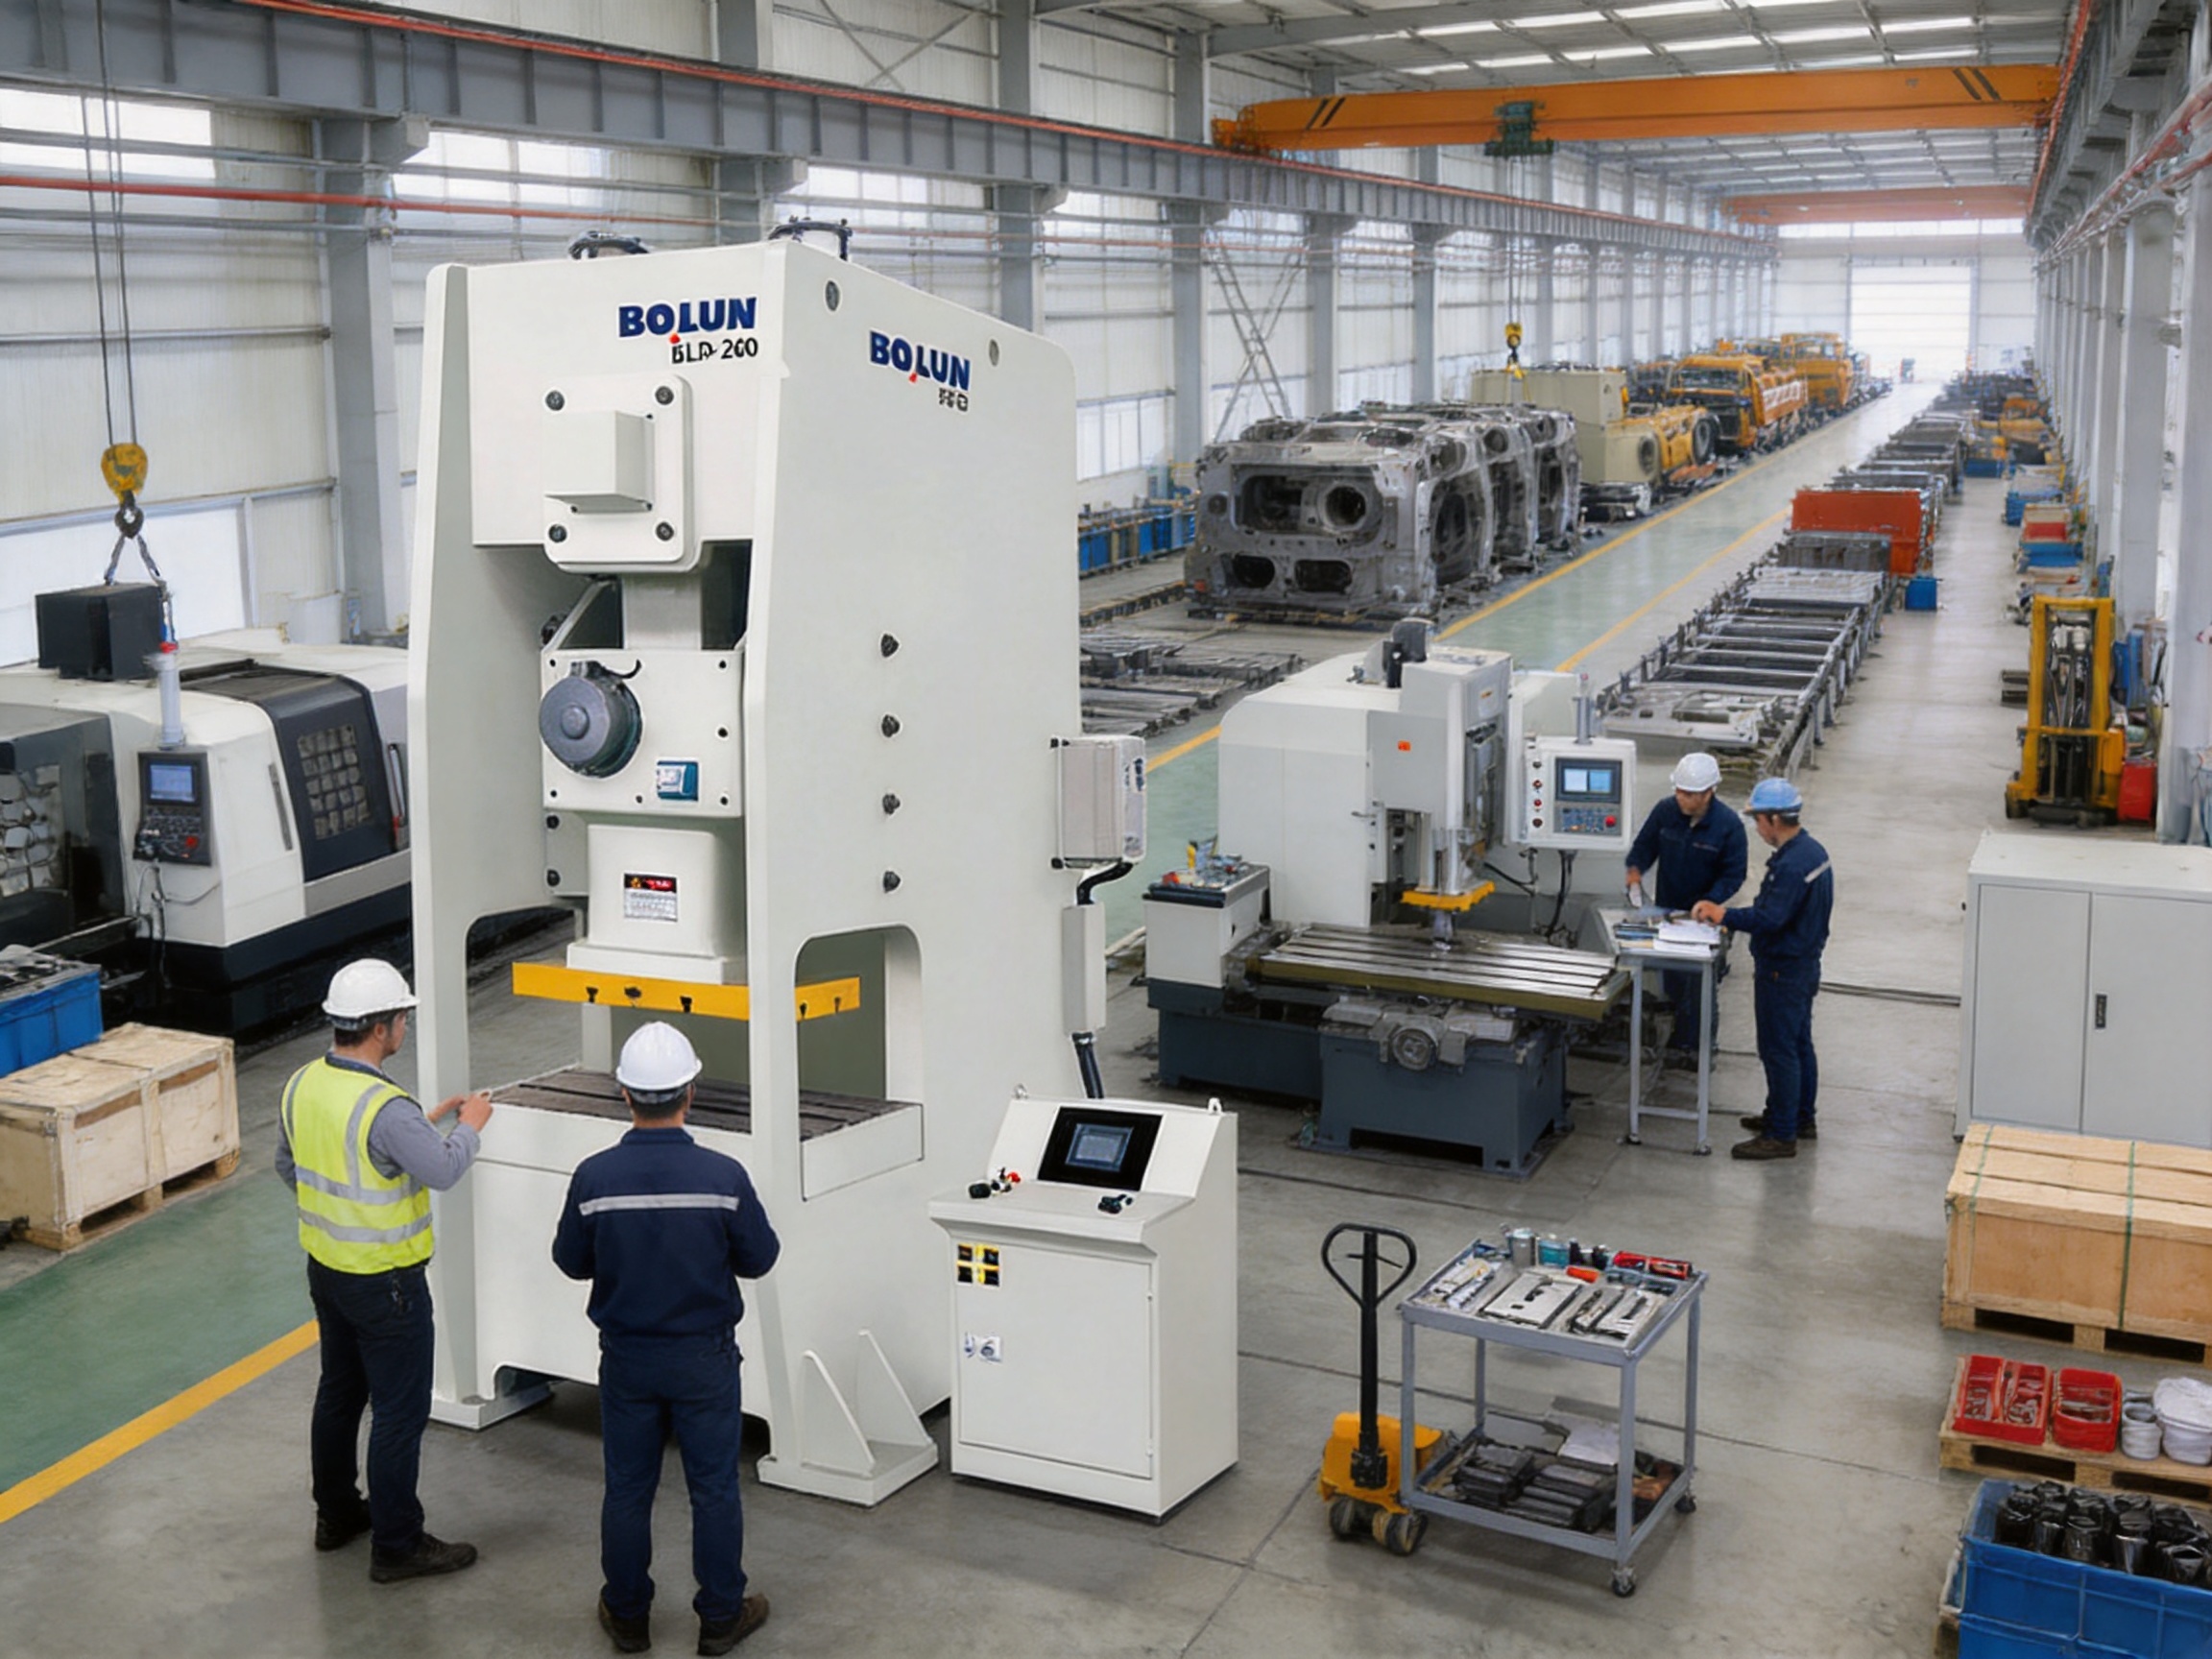
High-capacity power presses must be operated under a formal safety program. Operators should be trained in machine controls, die installation, material handling, emergency procedures, inspection requirements, and the hazards associated with stored mechanical and pneumatic energy.
Guarding and access controls must be correctly installed and maintained. The dual solenoid valve structure supports stopping control, but safe operation also requires suitable control logic, emergency-stop devices, protective guarding, and appropriate point-of-operation safeguards. The final safety arrangement must comply with the standards and regulations applicable in the customer’s location.
Before each production run, operators should verify die installation, fastener security, material position, lubrication, air pressure, abnormal noise, and display conditions. The tonnage monitoring system should be checked against the expected process range. Any unexpected increase in load should be treated as a reason to stop and investigate.
Operators should never bypass interlocks, remove guards during operation, or place hands within the die area while the machine is capable of cycling. Die changes, troubleshooting, and maintenance must follow documented lockout and isolation procedures. The main drive, pneumatic circuit, and other energy sources must be safely isolated before work begins.
Preventive maintenance is essential for preserving the advantages of a high-rigidity press. A maintenance program should include daily operator checks, scheduled lubrication inspections, periodic mechanical examinations, electrical inspections, safety-system tests, and accuracy verification.
Daily checks may include lubricant level, air pressure, unusual noise, abnormal vibration, oil leakage, fastener condition, stopping response, and tonnage display behavior. Operators should record abnormalities rather than relying on memory. Small changes often provide early warning of developing problems.
Weekly or monthly maintenance may include inspection of guide surfaces, die-height adjustment components, pneumatic valves, hoses, electrical cabinets, sensors, and control connections. The frequency should be adjusted according to operating hours, environmental conditions, production loads, and the manufacturer’s service recommendations.
Periodic accuracy checks can verify slide parallelism, repeatability, die-height positioning, table condition, and punch alignment. If a machine is used for precision forming, these measurements should be included in the factory’s quality-management system.
Hydraulic overload protection requires particular attention. The system should be inspected for leaks, correct pressure, response behavior, and calibration. Unauthorized changes to overload settings can compromise both safety and equipment protection.
The automatic lubrication system should be checked for reservoir level, pump operation, distribution-line integrity, filter condition, and lubricant suitability. A blocked line can create a hidden lubrication failure even when the pump appears to operate normally.
Maintenance should also include tooling. The best press cannot compensate for a damaged, poorly aligned, or incorrectly designed die. Die condition, guide pins, cutting edges, forming radii, cushion components, and fasteners should be inspected at defined intervals.
Productivity should be evaluated using the complete process rather than strokes per minute alone. A press may have a high nominal speed but deliver poor overall productivity if it causes frequent stoppages, difficult die changes, quality rejects, or accelerated tooling wear. The BLPD-260’s value comes from its ability to perform demanding operations with a combination of capacity, stroke, die space, monitoring, and protection.
The 22 kW motor provides the drive power required for the machine’s rated forming work. Actual energy consumption depends on cycle rate, load profile, motor efficiency, auxiliary equipment, lubrication, idle time, and production scheduling. Good process planning can reduce unnecessary idle operation and improve the utilization of each cycle.
Automatic lubrication and overload protection can contribute to lower maintenance-related downtime. Tonnage monitoring can help identify abnormal conditions before they develop into major failures. The large die space may reduce the need for repeated tooling modifications when product programs change. These benefits influence the total cost of ownership.
For manufacturers, the decision should consider purchase price, installation, foundation, tooling, training, maintenance, spare parts, energy, downtime, quality losses, and future product flexibility. A press that supports several product families may offer stronger long-term value than a lower-priced machine with limited capability.
Industrial press production involves many technical disciplines. Structural engineering determines the frame’s load path and stiffness. Mechanical engineering defines the drive, slide, crank, cushion, and adjustment mechanisms. Electrical and control engineering manage stopping, monitoring, and operator interaction. Manufacturing engineering establishes machining and assembly methods. Quality engineering verifies conformance. Service engineering supports the customer after delivery.
The company’s integrated structure brings these functions together. Its business covers R&D, design, production, sales, and service, allowing customer requirements to move through one coordinated organization. This can improve communication during specification, reduce misunderstandings, and simplify technical support.
Integrated production also benefits customized projects. If a customer requires a special die height, table arrangement, auxiliary interface, or process-monitoring function, the request can be evaluated by design and manufacturing teams together. This is more effective than treating customization as an isolated sales change.
The company’s stated technology-first strategy is supported by precision-processing equipment, core-component development, and an emphasis on full-chain production. These strengths are relevant to customers seeking equipment that must operate reliably in high-intensity industrial conditions.
Purchasing a large power press is a long-term industrial decision. Customers require more than a machine shipment. They need technical communication before purchase, documentation and coordination during production, installation support, commissioning assistance, operator guidance, and access to service after delivery.
The company provides a customer-oriented service system covering pre-sales consultation, in-sales support, and after-sales guarantees. Pre-sales consultation can help determine whether the nominal capacity, stroke, die height, table dimensions, cushion capacity, and speed range match the intended process.
During production and delivery, communication is important for confirming electrical standards, lifting points, foundation information, tooling interfaces, spare parts, and inspection requirements. After installation, technical support can help verify setup and optimize the machine for the customer’s actual material and die conditions.
International customers may also require documentation in formats suitable for internal approval, customs, installation, safety review, and maintenance planning. A manufacturer with an international management perspective is better prepared to coordinate with overseas production teams and technical departments.
Customers considering the BLPD-260 should begin with the workpiece and process rather than selecting a press only by product name. The required force should be calculated using material strength, thickness, perimeter, forming depth, friction, blank-holder force, and safety margin. The position of the maximum load should also be considered.
Next, the die dimensions should be compared with the worktable, slide bottom, column spacing, maximum die height, and adjustment range. The total die weight, center of gravity, mounting method, and lifting requirements should be confirmed.
Stroke and speed should be evaluated together. A 250 mm stroke may be essential for a deep component, but the required cycle rate must still be compatible with material feeding, forming time, part removal, and die protection. Customers should provide sample drawings, material specifications, production volume, and proposed die information to the manufacturer.
The cushion or mold pad requirements should be checked separately. The 140 kN capacity and 100 mm ram stroke may be suitable for many applications, but the actual force curve, effective area, timing, and die interface must be verified for each product.
Finally, the factory should evaluate installation conditions, foundation, power supply, compressed air, ventilation, operator access, automation, maintenance space, and safety compliance. A complete selection process reduces the risk of purchasing a machine that is technically powerful but poorly matched to the production environment.
It is a semi-closed single-point power press designed for deep forming, heavy-duty forging-related work, and large-scale industrial stamping. Its configuration combines a large working area with a rigid structure and a central single-point drive.
The nominal capacity is 2,600 kN. The actual suitability for a specific operation depends on the material, die, load position, forming method, and operating conditions. Engineering verification should be completed before production.
The 250 mm stroke provides greater vertical travel for deep drawing, deep forming, complex dies, and operations requiring additional clearance. It gives production engineers more flexibility than a short-stroke press when the component or die requires substantial movement.
The maximum die height is 550 mm, and the die-height adjustment range is 120 mm. These specifications support large tooling and provide flexibility when different dies are installed.
The worktable measures 1,140 by 840 by 180 mm. The slide bottom measures 1,130 by 650 by 100 mm. Customers should still verify die mounting details and effective working clearances for each tool.
The listed stroke range for the BLPD-260 vertical configuration is 20 to 40 strokes per minute. The appropriate production speed depends on material, die design, forming depth, lubrication, feeding, safety requirements, and quality objectives.
The main motor is listed as 22 kW in a four-pole configuration. It is selected to provide the torque required for the machine’s high-capacity forming work.
Yes. Hydraulic overload protection is integrated to help reduce the risk of serious damage caused by abnormal forming loads. It must be correctly adjusted and maintained, and it does not replace proper process engineering or safe operating limits.
Tonnage monitoring allows operators and production engineers to observe load conditions during operation. Changes in tonnage may indicate material variation, misfeeding, die wear, poor lubrication, or another abnormal condition.
Yes. Automatic lubrication helps deliver lubricant to designated components according to the machine’s operating requirements. The system still requires regular inspection, replenishment, and maintenance.
Yes. The listed mold pad capacity is 140 kN, with a 100 mm ram stroke and an effective cushion area of 810 by 480 mm. Final suitability depends on the die design and required force profile.
The product information lists GB/JIS Class 1 punch accuracy. Actual production accuracy will also depend on installation, die condition, material preparation, lubrication, maintenance, and operating practice.
Potential industries include automotive components, agricultural machinery, construction equipment, electrical products, appliances, industrial hardware, metal containers, structural parts, and other applications requiring high-force stamping or deep forming.
It may be suitable for selected heavy-duty forging-related applications, but forging loads can be highly dynamic. The material, temperature, die type, impact characteristics, and load profile must be reviewed with the manufacturer before selection.
Useful information includes part drawings, material type and thickness, production volume, forming process, die dimensions, required stroke, target cycle rate, automation needs, electrical standards, factory conditions, and any special safety or monitoring requirements.
The producer integrates research and development, design, precision processing, production, assembly, inspection, sales, customization, and service. It also emphasizes full-chain production, non-standard equipment development, technological innovation, and quality control.
The BLPD-260 Industrial Strength Deep-Stroke Semi-Closed Single-Point Power Press is designed for manufacturers that require more than basic stamping capacity. Its 2,600 kN nominal force, 250 mm slide stroke, 550 mm maximum die height, 32-ton rigid structure, large worktable, and cushion-support capability create a strong platform for deep forming and heavy industrial production.
Its competitive value comes from the combination of features. The machine offers deep travel without abandoning the repeatability of a mechanical power press. It provides large die space while retaining a practical semi-closed configuration. It combines a high-torque 22 kW drive with hydraulic overload protection, automatic lubrication, tonnage monitoring, and dual solenoid valve stopping control.
The equipment is supported by a manufacturer with experience in machinery development, precision processing, integrated production, customized design, inspection, and customer service. These manufacturing strengths are important because the long-term performance of a large press depends on much more than its catalog specifications. Structural accuracy, assembly quality, commissioning, maintenance, and technical support all influence the final return on investment.
For customers seeking a reliable high-capacity press for large dies, deep forming, heavy blanking, and demanding industrial stamping, the BLPD-260 provides a technically substantial option. A final purchase decision should be based on detailed process calculations, die compatibility, installation conditions, safety requirements, and consultation with the manufacturer. When correctly matched to the application and properly maintained, the machine can serve as a durable foundation for efficient, stable, and high-quality metal forming.
1. Product technical information for the BLPD-260 Industrial Strength Deep-Stroke Semi-Closed Single-Point Power Press.
2. General principles of mechanical power press design, operation, and maintenance.
3. Industrial metal-forming process engineering practices for stamping, blanking, bending, and deep drawing.
4. Guidance on hydraulic overload protection and press-load monitoring systems.
5. General requirements for machine installation, foundation preparation, die setup, and preventive maintenance.
6. GB and JIS precision classifications applicable to press machinery and punching accuracy.
7. Industrial safety principles for power presses, point-of-operation protection, emergency stopping, and energy isolation.


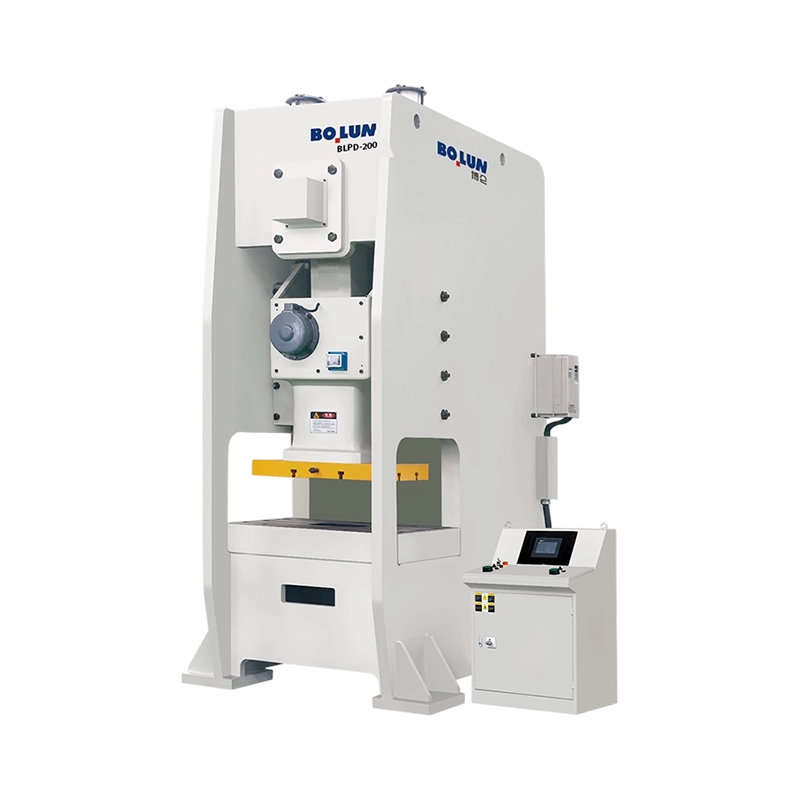
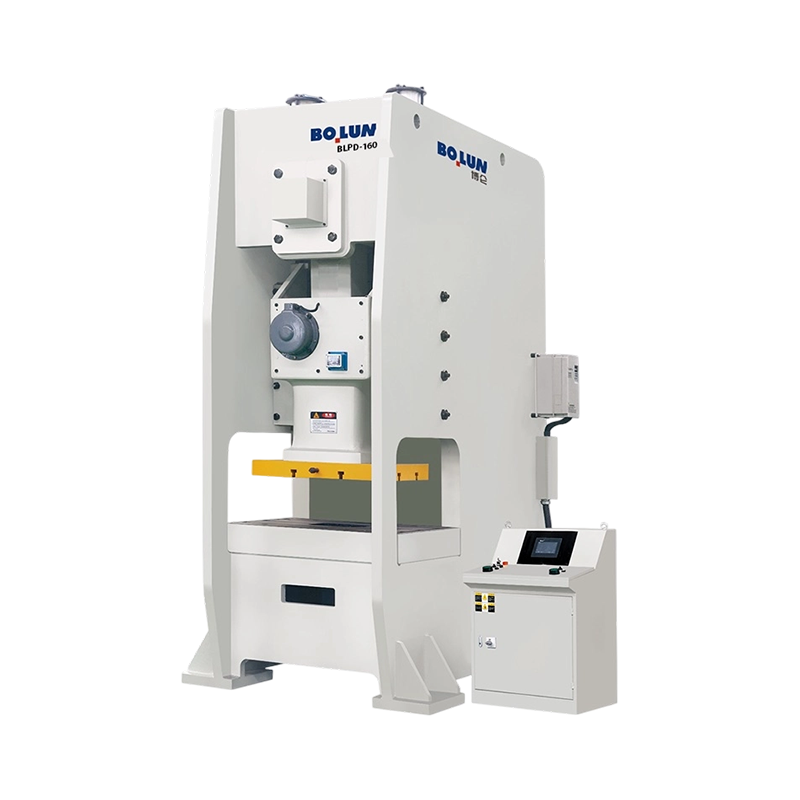
Two presses can both carry a 200-tonne nameplate and still produce very differe...
Start With the Purchase Decision, Not the Definitions A procurement engineer co...
What Is a Power Press? A power press — also called a stamping press or punch pr...
A tooling engineer quotes a new bracket program and specifies a 160-ton press. ...
When you are planning to produce medium or small metal parts in high volumes, t...
A fastener plant in Taizhou receives a request from an automotive tier-one supp...
Contact Us

topbolun@gmail.com

+86-575-83362228

+86-13735238388
+86-18667502750

+86-575-83362999

+8618667502750

No.1 Linjiang Road East, Xiaren, Jinting Town, Shengzhou City, Zhejiang Province, China
Ready to Begin?
Get in Touch

Now!

ZHEJIANG BOLUN
 English
 中文简体