Modern stamping operations require more than high nominal tonnage. Manufacturers must also control forming energy, manage complex die movements, maintain repeatable quality, reduce setup time, and protect valuable tooling. These requirements become especially demanding when processing thick sheet, high-strength materials, automotive components, appliance parts, and other large workpieces. A power press designed only for force may complete a forming cycle, but it may not deliver the precision, flexibility, monitoring capability, and production stability required in a competitive manufacturing environment.
The BLAS-160 Heavy-Duty Programmable Motion Open-Type Single-Point Servo Power Press is designed for this demanding segment of the market. With a nominal capacity of 1,600 kN and a maximum continuous working energy of 9,000 J, it provides the force and energy reserve necessary for high-load stamping and stable forming of thick materials. Its 1,200 × 760 mm worktable accommodates substantial dies, while its 720 × 580 mm slide bottom provides a practical mounting area for heavy-duty tooling.
Unlike a conventional fixed-motion mechanical press, the machine uses a servo-driven system to provide programmable slide movement. This enables manufacturers to adjust the motion profile according to material behavior, die requirements, and production objectives. The result is a more adaptable forming platform for operations that may include blanking, bending, shallow drawing, embossing, coining, trimming, and other precision stamping processes.
The equipment is manufactured by Zhejiang Bolun High-Precision Machinery Co., Ltd., a Chinese industrial machinery company with experience in research and development, engineering design, production, sales, and technical service. The company combines precision processing, non-standard customization, structured quality control, and application-oriented engineering to serve customers in demanding forming industries.
This article examines the design, working capabilities, technical advantages, manufacturing strengths, application value, and selection considerations associated with this heavy-duty open-type servo power press.
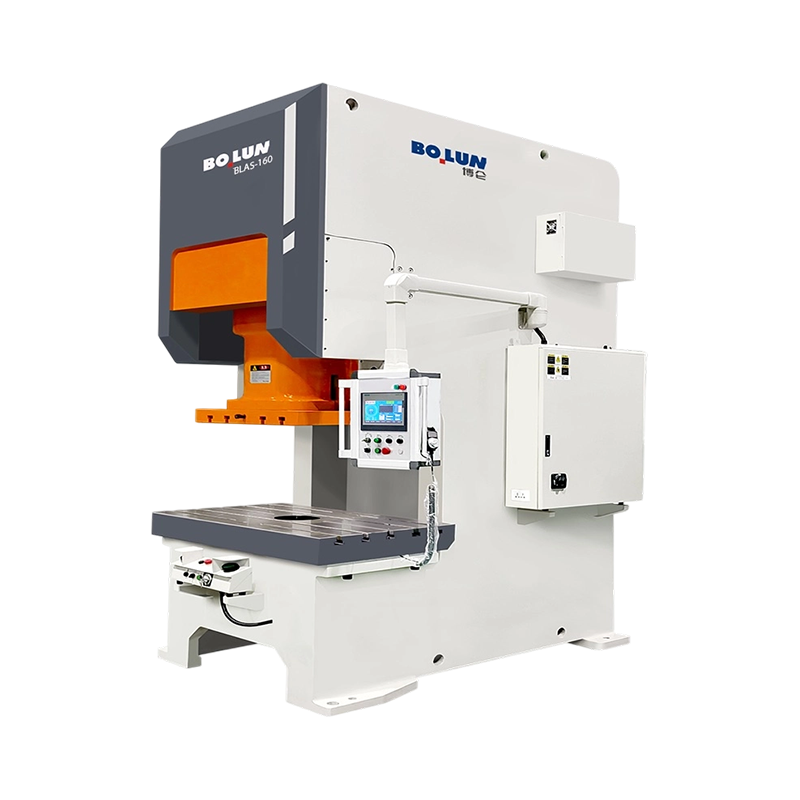
BLAS-160 Heavy-Duty Digital-Forming Open-Type Single-Point Servo Power Press
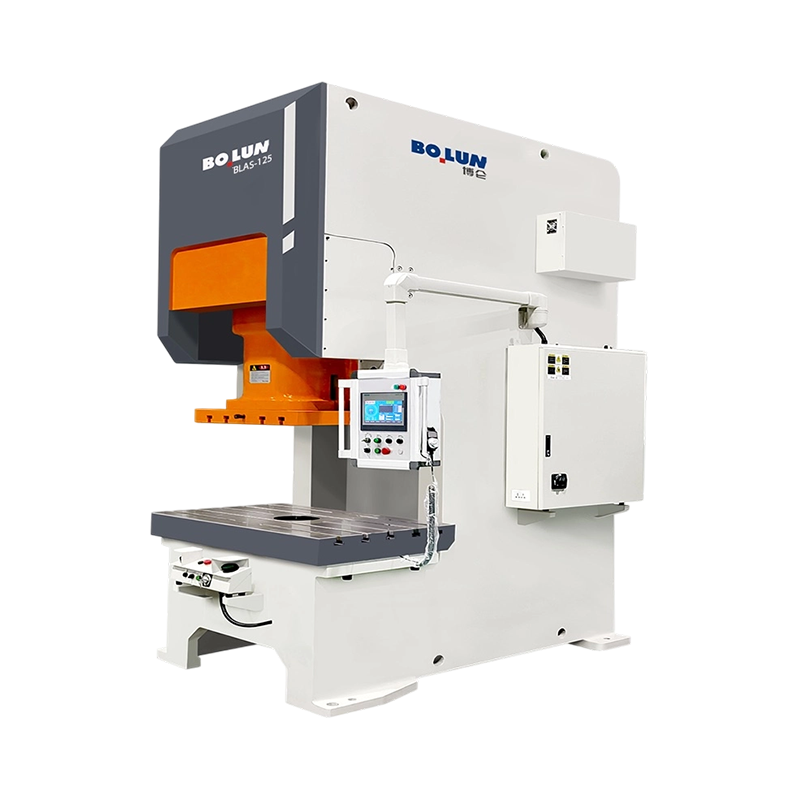
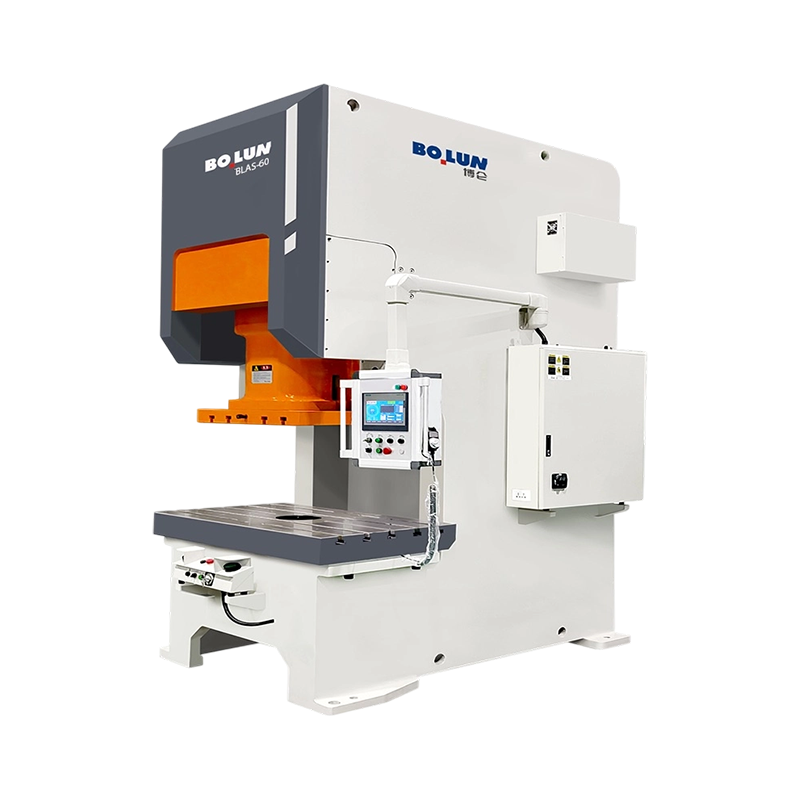
The machine belongs to the open-type single-point servo power press category. This configuration combines a rigid stamping frame with an open-front working area. The open structure allows operators and automated equipment to access the die zone from the front, which is particularly useful for loading, unloading, die inspection, part transfer, and integration with feeding systems.
The single-point drive arrangement concentrates slide movement through a central transmission point. This design is commonly selected for general-purpose stamping because it offers a practical balance between structural strength, tooling accessibility, operating simplicity, and production versatility. For a 1,600 kN press, maintaining alignment between the slide, die, and worktable is essential. The machine’s structural arrangement is intended to support stable force transfer during demanding cycles.
The heavy-duty designation reflects the machine’s capacity, energy rating, die accommodation, and overall application range. Its nominal capacity of 1,600 kN places it well above light and medium stamping equipment. This provides additional process headroom for materials and operations that would be unsuitable for smaller machines. A press should not normally be operated continuously at its absolute limit, so the higher capacity can also provide a useful margin for process stability and die protection.
The programmable motion concept is another important aspect of the machine. A servo-driven slide can be controlled with greater flexibility than a traditional fixed-speed crank motion. Depending on the selected program, the slide can be configured for different approach, forming, dwell, return, and transfer conditions. This is valuable when the material requires a controlled forming speed or when the die includes multiple stages with different motion demands.
Stored die parameters can help standardize production between batches. Once a suitable motion profile and operating configuration have been developed, the information can be retained for repeat jobs. This reduces reliance on manual adjustment and supports more consistent changeovers, particularly in factories producing multiple components on the same machine.
With 1,600 kN of nominal capacity, the press is appropriate for applications where substantial forming force is required. Examples may include medium-to-large automotive brackets, structural panels, appliance components, electrical enclosures, industrial covers, reinforcement parts, and formed components made from relatively thick sheet.
Capacity alone does not determine whether a press is suitable for a particular job. Die size, shut height, slide dimensions, throat depth, energy requirements, material characteristics, and production speed must all be considered. The BLAS-160 configuration addresses these factors with a 400 mm maximum die height, 100 mm die height adjustment, 390 mm throat depth, and a 1,200 × 760 mm worktable.
The open-front arrangement improves visibility around the die area. Operators can observe material positioning, part release, and tooling conditions more easily than with a fully enclosed frame. The design also supports mechanical or robotic part handling systems that approach from the front.
Open access is especially helpful during setup and maintenance. Die alignment, trial stamping, inspection, and adjustment can be completed with a clearer view of the working zone. When combined with a color touch-screen HMI, this arrangement contributes to a more accessible and manageable production environment.
The following table summarizes the principal specifications of the 1,600 kN configuration. These values should be reviewed together with the actual die design, material requirements, safety conditions, and customer-specific configuration before equipment selection.
| Specification | Value |
|---|---|
| Product model | BLAS-160 |
| Press type | Open-type single-point servo power press |
| Nominal capacity | 1,600 kN |
| Nominal stroke | 5 mm |
| Continuous working energy | 9,000 J |
| Slide stroke | 200 mm |
| Strokes per minute | Approximately 50 S.P.M. |
| Maximum die height | 400 mm |
| Die height adjustment | 100 mm |
| Throat depth | 390 mm |
| Worktable size | 1,200 × 760 × 150 mm |
| Slide bottom size | 720 × 580 × 90 mm |
| Distance between columns | 750 mm |
| Working face height | 915 mm |
| Shank hole diameter | 65 mm |
| Die height adjustment motor | 1.1 kW |
| Cushion capacity | 100 kN |
| Cushion working stroke | 80 mm |
| Effective cushion area | 540 × 350 mm |
| Punch accuracy | JIS B 6402 Level 1 |
| Required air pressure | 0.55 MPa |
The 200 mm slide stroke provides a useful range for many forming operations. The approximately 50 strokes-per-minute rating offers a balance between productivity and the controlled motion required for heavier work. Actual production speed depends on the selected motion program, stroke length, material, die complexity, feeding method, part geometry, and safety requirements.
The 9,000 J continuous working energy specification is particularly relevant to production planning. It indicates the energy available for repeated operation under defined conditions. Engineers should compare the required forming energy of a specific die with the machine’s continuous energy capability rather than relying only on peak tonnage.
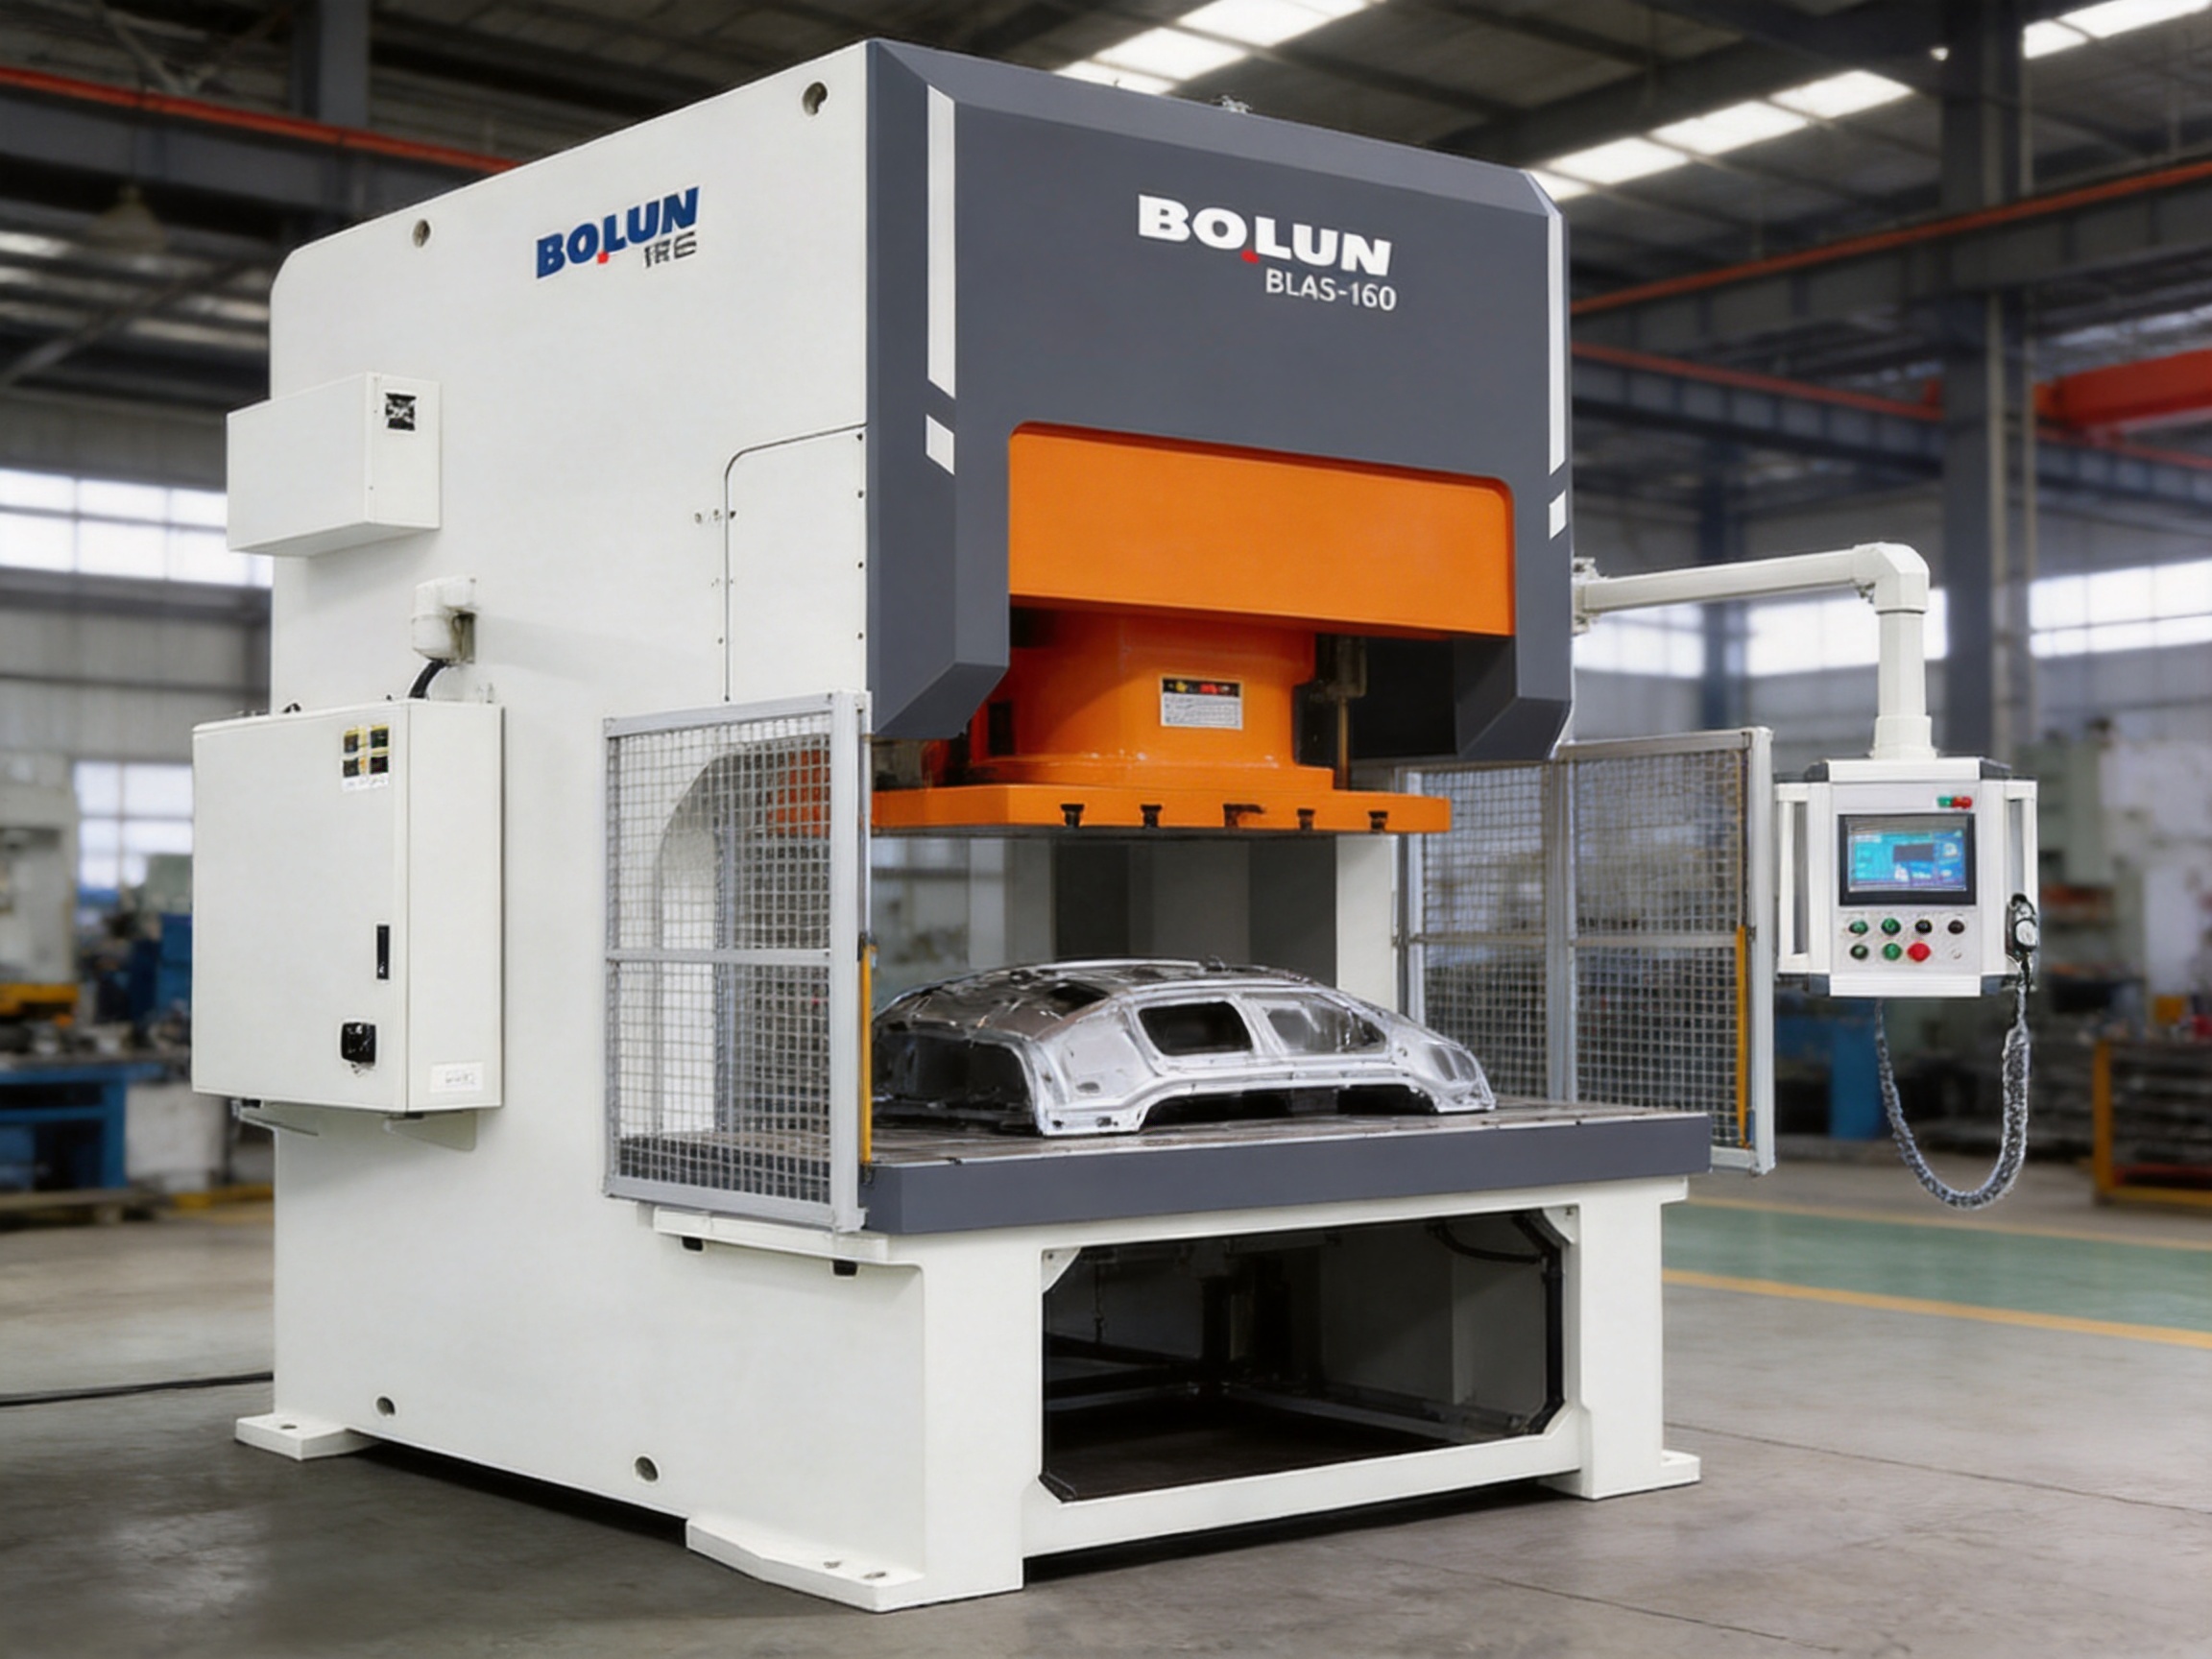
The primary technical advantage of a servo power press is the ability to control slide motion more flexibly. In a traditional mechanical press, the slide follows a largely predetermined motion based on crank geometry and drive speed. While this arrangement remains effective for many operations, it may not be ideal for every material or forming sequence.
A programmable servo system can support multiple motion strategies. The slide may approach the workpiece at a higher speed, slow down during the forming zone, dwell briefly at the bottom of the stroke, and return according to a selected profile. These functions can be adapted to material flow, die clearance, lubrication, springback behavior, and part geometry.
Forming speed can influence material flow, surface quality, tool loading, and the risk of defects. Some materials benefit from a slower and more controlled forming stage, while other operations require faster movement during non-forming sections of the cycle. Programmable servo motion allows the process engineer to separate these phases more effectively.
For thick material, a controlled forming speed can help reduce shock loading and improve the stability of the die engagement. In applications involving bending or drawing, the motion profile may be adjusted to support smoother material movement. This can contribute to more consistent parts and reduced stress on tooling, although final results always depend on die engineering and process validation.
A programmable dwell can be useful in operations where material must remain under pressure for a controlled interval. Examples may include coining, flattening, embossing, calibration, and certain forming processes requiring improved dimensional definition.
Holding the slide near the bottom position can also assist with repeatability. The correct dwell time and position depend on the material, die construction, required tolerance, and production cycle. The machine’s programmable architecture gives users a practical method for testing and storing these process settings.
Conventional presses may require substantial mechanical or operational adjustment when a new die is installed. A servo press can move more of the process definition into the control system. Parameters such as motion profile, speed zones, stopping position, and operating sequence can be associated with a die or product program.
This does not eliminate the need for correct die setup. Mechanical alignment, shut height, lubrication, material feeding, and safety checks remain essential. However, programmable control can make the repeatable portion of the setup more systematic and reduce the possibility of inconsistent manual settings between production shifts.
The integrated tonnage monitoring system is designed to provide real-time feedback about load conditions during stamping. This function is important because a press may experience different force patterns depending on material thickness, hardness, lubrication, die wear, feeding accuracy, and part geometry.
Monitoring load behavior can help operators identify abnormal conditions before they develop into severe equipment or tooling damage. A sudden increase in force may indicate misfeeding, double-sheet loading, a blocked part, incorrect die height, insufficient clearance, or a tooling problem. Early detection supports faster intervention and can reduce unplanned downtime.
Load monitoring can also assist with quality control. When a stable process produces a recognizable force profile, deviations from that profile may indicate a change in material or forming conditions. The information can be used alongside dimensional inspection and visual checks to strengthen production control.
The color touch-screen HMI provides an interface for observing operating data and adjusting permitted process parameters. A clear HMI is valuable in a high-capacity machine because it helps operators understand the selected program, operating status, alarms, and machine conditions.
Process data can support several production objectives:
First, it can improve repeatability by allowing approved parameters to be stored and recalled. Second, it can help maintenance personnel distinguish between normal wear and sudden process abnormalities. Third, it can support troubleshooting by providing information about when a problem occurred. Fourth, it can provide a foundation for future integration with factory monitoring or production management systems, subject to the final machine configuration.
Manufacturers should establish clear procedures for alarm response, parameter authorization, and data review. The monitoring system is most effective when it is integrated into a broader quality management process rather than treated as a standalone protection device.
The machine’s worktable measures 1,200 × 760 mm, with a listed thickness of 150 mm. This provides a broad and substantial mounting surface for large dies used in automotive, appliance, electrical, and general industrial applications.
The 720 × 580 mm slide bottom provides a suitable interface for upper die mounting. Together, the worktable and slide dimensions allow the press to accommodate tooling that would exceed the practical range of smaller machines. The distance between columns is 750 mm, giving the operator and tooling designer useful lateral space within the open frame.
The maximum die height is 400 mm, while the die height adjustment range is 100 mm. This combination enables the machine to accept dies with different closed heights and provides adjustment flexibility during setup. Engineers should confirm the complete die stack, including upper and lower die plates, material lifters, cushions, guides, sensors, and any feeding or transfer equipment.
The 390 mm throat depth is another important selection factor. It defines how far the working area extends from the front of the frame toward the drive structure. A deeper throat can be beneficial for parts with larger forming areas, but the actual suitability depends on the location of the forming load and the stiffness requirements of the die.
Heavy dies require a properly planned installation method. The press should be equipped and operated according to the manufacturer’s instructions, with attention to lifting capacity, die positioning, clamping, slide movement, and safety isolation. The table and slide dimensions help define the physical envelope, but die weight and center of gravity must also be evaluated.
For manufacturers operating multiple products, the ability to store die-related parameters can help shorten setup time. A structured changeover procedure may include selecting the correct program, confirming die height, verifying material specifications, checking sensors, testing low-speed motion, and conducting a first-piece inspection.
The press is equipped with a cushion rated at 100 kN, with an 80 mm working stroke and an effective area of 540 × 350 mm. A cushion can provide support from below the workpiece during selected forming processes. It may assist with blank holding, reverse forming, controlled material movement, or part ejection, depending on the die configuration.
The cushion’s capacity and working stroke must be matched to the intended operation. A cushion is not simply an additional force source; it is part of the forming system. Its timing, position, force, and interaction with the upper die can influence material flow and final part quality.
For shallow drawing and other controlled forming applications, a cushion can help maintain more consistent conditions from cycle to cycle. For complex tooling, engineers may need to validate the cushion force curve, contact area, return behavior, and synchronization with the servo slide.
The effective cushion area of 540 × 350 mm gives die designers a defined region for applying support. The actual contact arrangement should be considered during die development to avoid uneven loading or interference with ejectors, punches, sensors, and other components.
The listed punch accuracy is JIS B 6402 Level 1. This indicates that the machine is designed according to a recognized precision standard for press performance. Accuracy is influenced by many factors, including frame rigidity, slide guidance, drive condition, die alignment, foundation quality, lubrication, operating temperature, and maintenance.
A heavy-duty press must resist deformation under high load. If the frame or slide deflects excessively, the die may experience uneven loading, accelerated wear, dimensional variation, or premature failure. Structural design and precision manufacturing therefore play a central role in the machine’s long-term performance.
Stable operation also depends on appropriate installation. The foundation must be capable of supporting the machine’s static and dynamic loads. Leveling, anchoring, vibration control, electrical supply, air supply, and working clearance should be addressed before commissioning.
The machine’s working face height of 915 mm supports a practical operator interface while allowing room for die handling and feeding arrangements. The final ergonomic suitability depends on factory layout, platform requirements, guarding, and the selected automation system.
High force magnifies the effects of small alignment errors. A minor deviation in die positioning can create uneven contact across the tool, concentrating load in a limited area. Over time, this may damage inserts, punches, guide components, or die plates.
Precision is therefore not only a matter of finished-part accuracy. It also supports tooling protection, predictable maintenance intervals, reduced scrap, and stable operating costs. The combination of a rigid heavy-duty structure, controlled motion, and monitoring capability provides a stronger foundation for consistent production than force capacity alone.
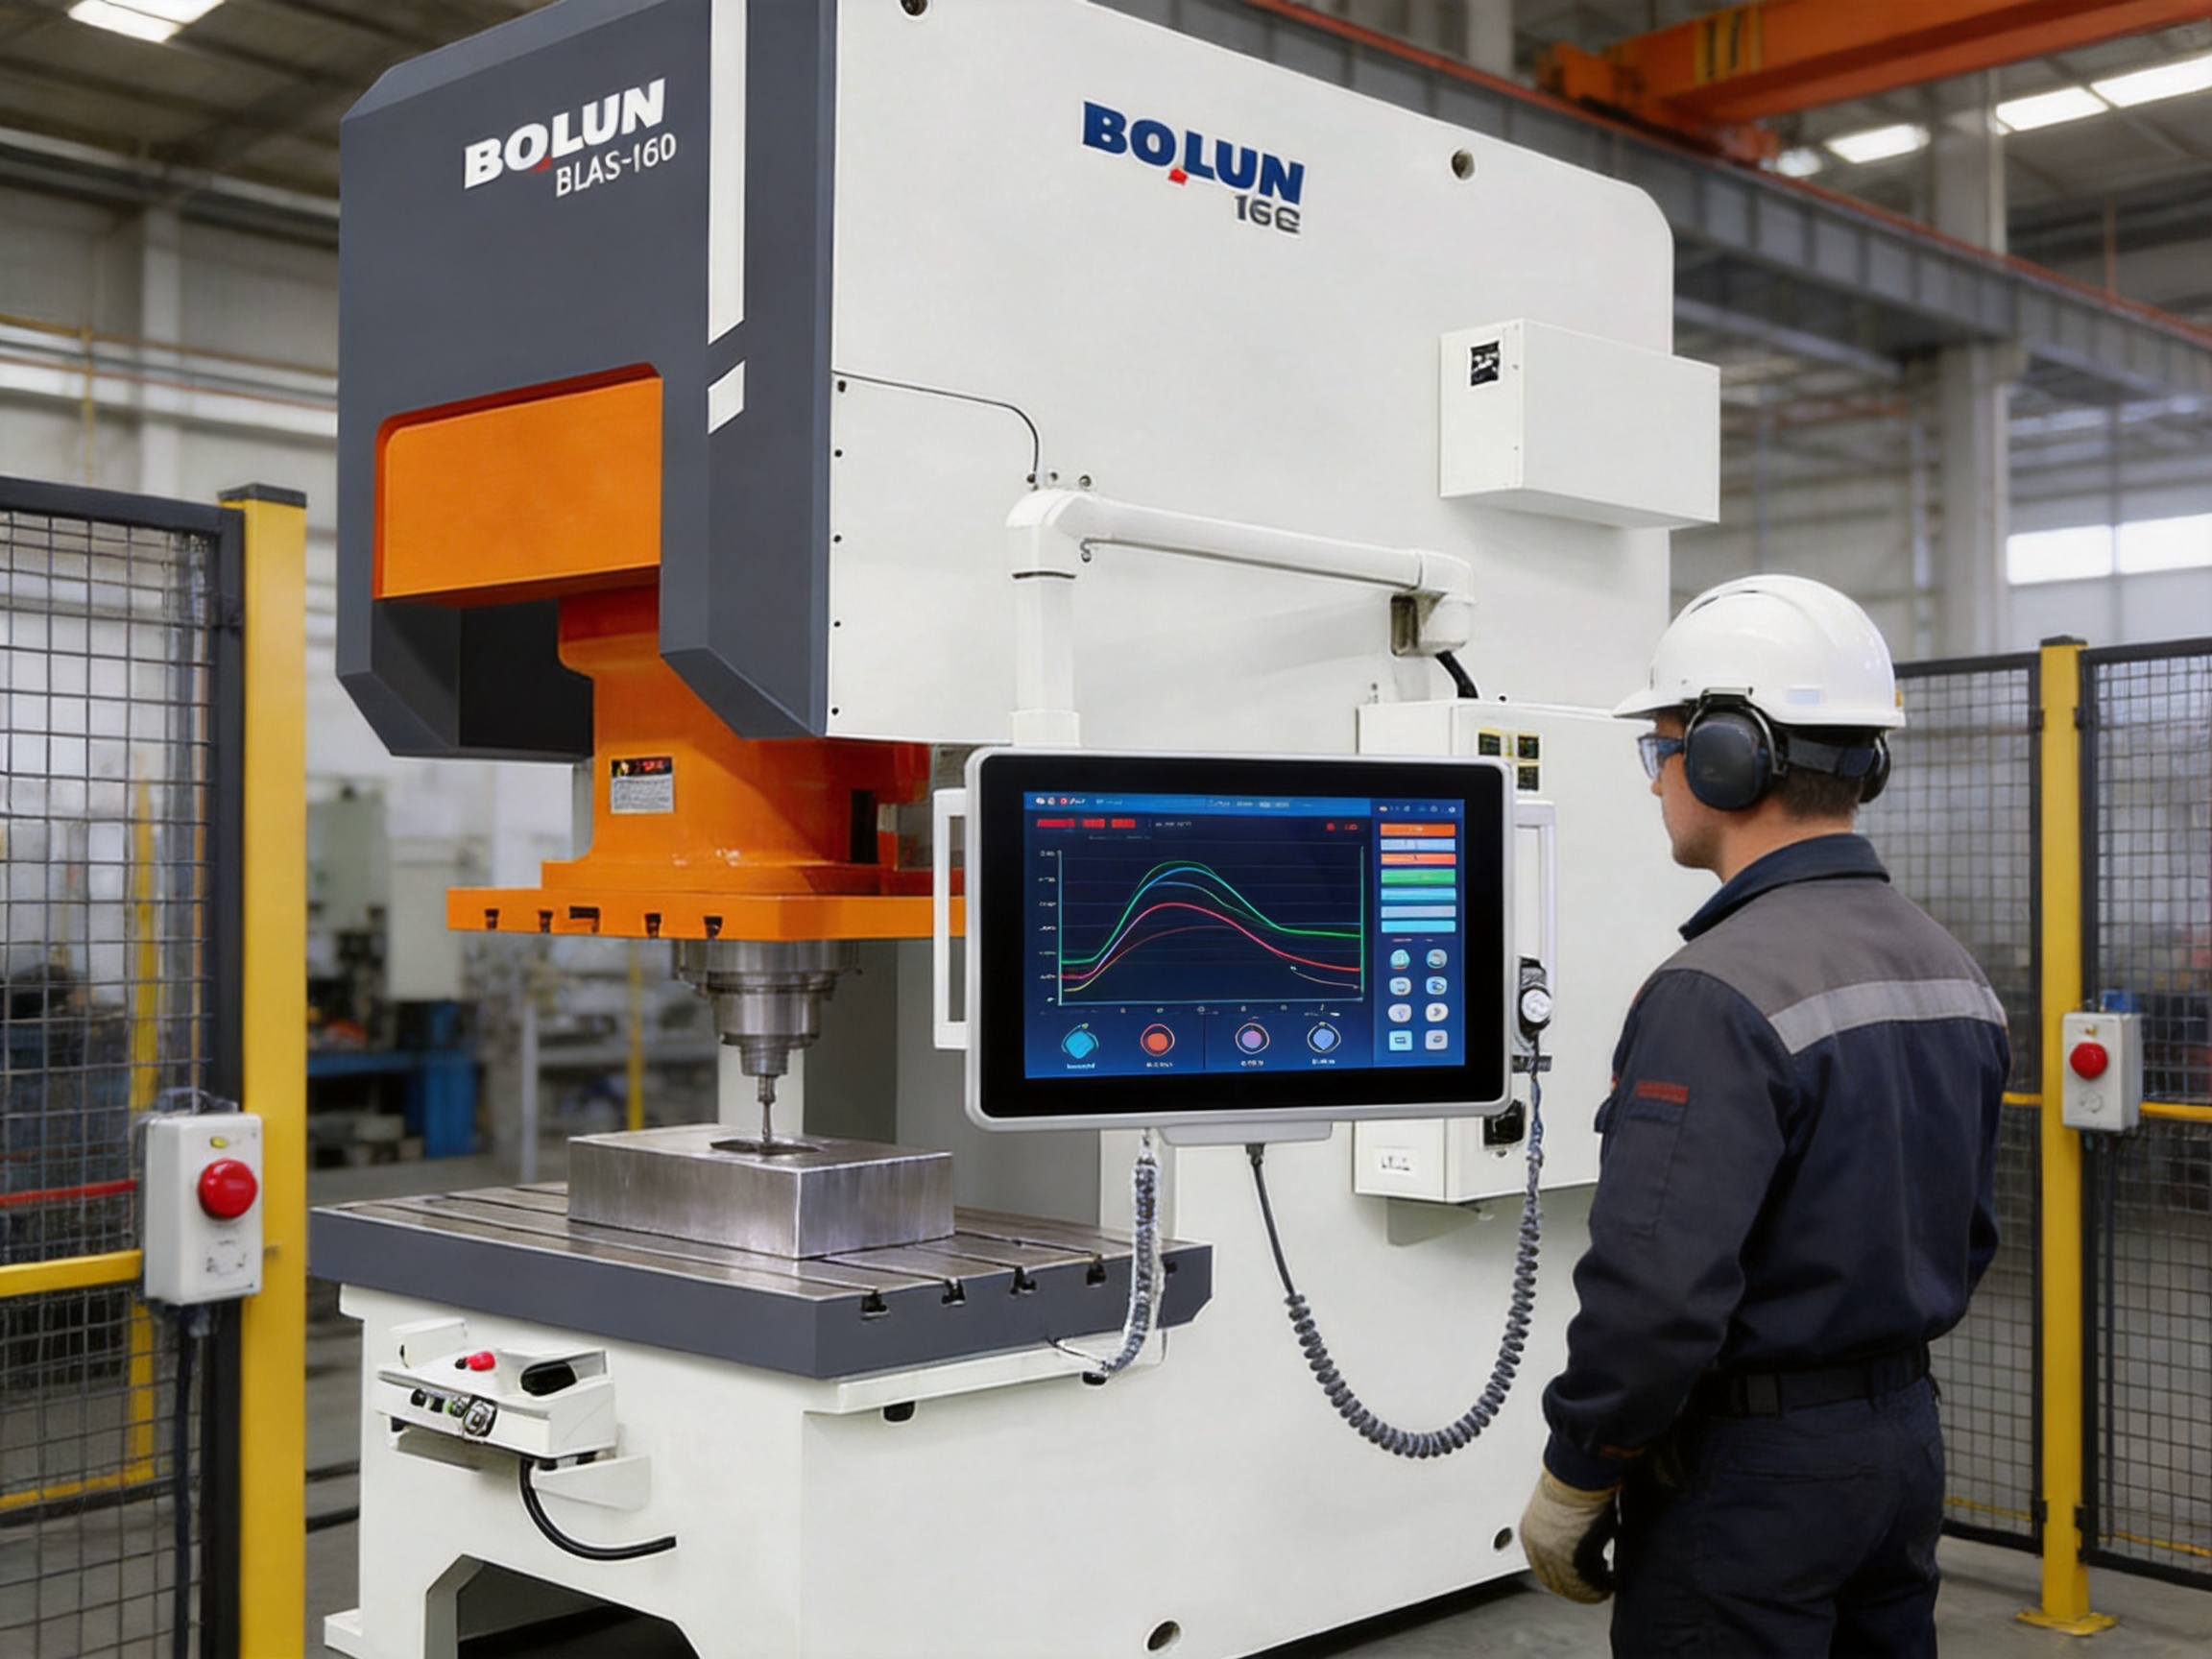
Manufacturers evaluating a new press commonly compare it with traditional mechanical presses, smaller servo presses, and other high-capacity machines. The most important advantages of this configuration relate to process flexibility, useful workspace, monitoring, and application range.
A standard mechanical press may provide excellent productivity for a narrow range of repetitive operations, but its fixed motion can limit optimization for difficult materials and complex dies. The programmable servo system allows users to adjust slide speed and sequence according to the job. This can provide better control when the forming process requires slow engagement, bottom dwell, or specialized return behavior.
Smaller presses may offer lower acquisition and operating costs, but they can be unsuitable for large dies, thick sheet, or high-force operations. The 1,600 kN rating and 9,000 J continuous working energy give this machine a stronger capability envelope. Users can select a press with sufficient reserve instead of operating a smaller machine near its limits.
The 1,200 × 760 mm worktable and 720 × 580 mm slide bottom support larger tooling than many compact open-type presses. This can reduce the need to split an operation across several machines or use undersized dies that restrict part geometry.
Tonnage monitoring and HMI-based control provide a clearer view of machine behavior than a basic press with limited feedback. Operators and engineers can respond to load deviations, confirm program selection, and manage process parameters more systematically.
Many factories no longer produce only one high-volume component. They may manufacture several part families in different materials and thicknesses. A programmable press can be more useful in this environment because its motion profile can be adapted from one die to another. Stored parameters also support repeat production after an order returns to the factory.
These advantages should not be interpreted as a guarantee that the machine will outperform every competing press in every application. Press selection depends on actual production volume, die design, automation, energy consumption, floor space, service support, and total cost of ownership. The value of this configuration is strongest where capacity and flexibility are both required.
The company behind the machine combines industrial machinery research and development, design, manufacturing, sales, and service. Its stated experience spans approximately two decades in machinery manufacturing, with a focus on forging, casting, and precision forming equipment.
A major strength is the company’s integrated production approach. Instead of relying only on final assembly, it emphasizes a full-chain system covering basic design, core component development, precision processing, machine assembly, inspection, and service. This type of integration can improve communication between engineering and production teams and provide better control over critical machine characteristics.
High-capacity presses require components that are manufactured and assembled with consistency. Frame sections, slides, tables, guide structures, drive components, and adjustment mechanisms must work together within defined tolerances. Advanced precision processing equipment can help the manufacturer produce and inspect these components more reliably.
Precision processing is particularly important for large parts because dimensional errors can become difficult and expensive to correct after assembly. A coordinated manufacturing system helps reduce the risk of mismatched components and supports more predictable machine performance.
Industrial customers often require more than a standard catalog configuration. They may need special die interfaces, feeding systems, different safety arrangements, customized control logic, additional monitoring, or integration with existing production lines.
The company provides non-standard customization and one-stop design and manufacturing services for products with special specifications and functions. This capability can be valuable for customers whose parts, dies, factory layouts, or production sequences do not fit a standard machine package.
The company describes quality as a central part of its operating philosophy. Its finished-product inspection system is intended to exceed basic industry requirements by checking components and processes throughout production rather than relying only on a final inspection.
For a heavy-duty press, quality control may include dimensional verification, component inspection, assembly checks, electrical testing, control-system validation, lubrication review, trial operation, and performance confirmation. The exact inspection plan depends on the final configuration and applicable customer requirements.
A process-based quality system is preferable to a purely visual final check because it helps identify issues earlier. It also creates a more traceable manufacturing history and supports corrective action when a deviation is detected.
Press equipment is a long-term production asset. Its value depends not only on initial performance but also on commissioning, operator training, spare parts, troubleshooting, preventive maintenance, and technical response. The company presents its service system as covering pre-sales consultation, in-sales support, and after-sales guarantees.
Pre-sales support can help customers define capacity, die dimensions, automation requirements, and utility conditions. During delivery and commissioning, technical support can assist with installation, parameter setup, and trial production. After installation, service resources can help maintain reliability and protect the customer’s investment.
The press is suited to a wide range of high-load stamping applications. Automotive component production is one important area because vehicle parts often require substantial forming force, controlled material flow, and repeatable die operation.
Possible automotive applications include brackets, reinforcement members, structural supports, mounting components, chassis-related parts, and other medium-to-large stamped components. The exact suitability depends on part size, material grade, forming depth, required accuracy, and die construction.
Appliance manufacturing is another potential application. The large worktable can support dies used for panels, internal structural parts, mounting plates, housings, and reinforcement components. Servo motion may be useful when surface appearance, controlled deformation, or multiple material conditions must be managed.
Electrical and industrial equipment manufacturers may use the press for enclosures, covers, brackets, frames, and formed sheet-metal components. In these sectors, the ability to store different programs can support mixed production and frequent product changes.
General metalworking companies may also benefit from the machine’s flexible architecture. It can serve as a central production asset for blanking, bending, embossing, shallow drawing, calibration, and other operations that fall within its force, energy, stroke, and die-size limits.
Materials may include carbon steel, stainless steel, coated sheet, aluminum alloys, and other formable metals. However, material suitability must be established through engineering analysis and trials. Tensile strength, yield strength, thickness, ductility, lubrication, grain direction, and springback all affect the required force and motion profile.
The machine’s high capacity does not remove the need to calculate forming load. A die that requires excessive force, energy, or eccentric loading can damage both tooling and equipment. Customers should provide complete material and part data during the quotation and engineering stages.
Productivity is not determined only by strokes per minute. A press that operates quickly but produces inconsistent parts, frequent die damage, or lengthy setup delays may have a higher overall cost than a slightly slower machine with better process stability.
The approximately 50 S.P.M. rating provides a useful production capability for a heavy-duty 1,600 kN press. Servo control may help optimize the cycle by allowing faster movement in non-forming portions while maintaining controlled speed during critical forming stages. The actual cycle time should be calculated using the complete sequence, including feeding, part transfer, inspection, lubrication, and operator access.
Stored programs can reduce repeated setup work. If a die is used regularly, recording approved parameters can improve consistency between production runs. This may reduce trial pieces, shorten start-up time, and make shift-to-shift operation more uniform.
Tonnage monitoring can also contribute to cost control. Detecting abnormal loads earlier may help prevent expensive die damage and minimize scrap. In addition, process data can support maintenance planning by showing changes in load behavior that may indicate wear or alignment problems.
Energy performance depends on the complete servo system, operating profile, production load, and facility conditions. Customers should request final power and utility data for the exact machine configuration when preparing a factory installation plan.
A high-capacity power press must be installed and operated under a formal safety program. Operators should receive training in machine controls, die setup, emergency procedures, guarding, lockout and isolation, and abnormal-condition response.
The installation area should provide sufficient clearance for die handling, material loading, part removal, maintenance access, and safe movement around the press. The floor and foundation must be checked for load-bearing capability and stability. Utility connections, including electrical supply and compressed air at approximately 0.55 MPa, should be prepared according to the final technical documentation.
Preventive maintenance should include lubrication, inspection of guide and drive components, checking of fasteners, examination of electrical cabinets, verification of sensor operation, review of air-system condition, and confirmation of safety functions. The exact intervals should follow the manufacturer’s maintenance recommendations and the intensity of use.
Die maintenance is equally important. A well-maintained machine cannot compensate for damaged, misaligned, poorly lubricated, or improperly installed tooling. The press, die, material feed, lubrication system, and quality inspection process should be managed as one production system.
When a tonnage alarm or abnormal load condition occurs, the operator should follow an established procedure rather than simply resetting the alarm. The cause should be investigated, documented, and corrected before normal production resumes.
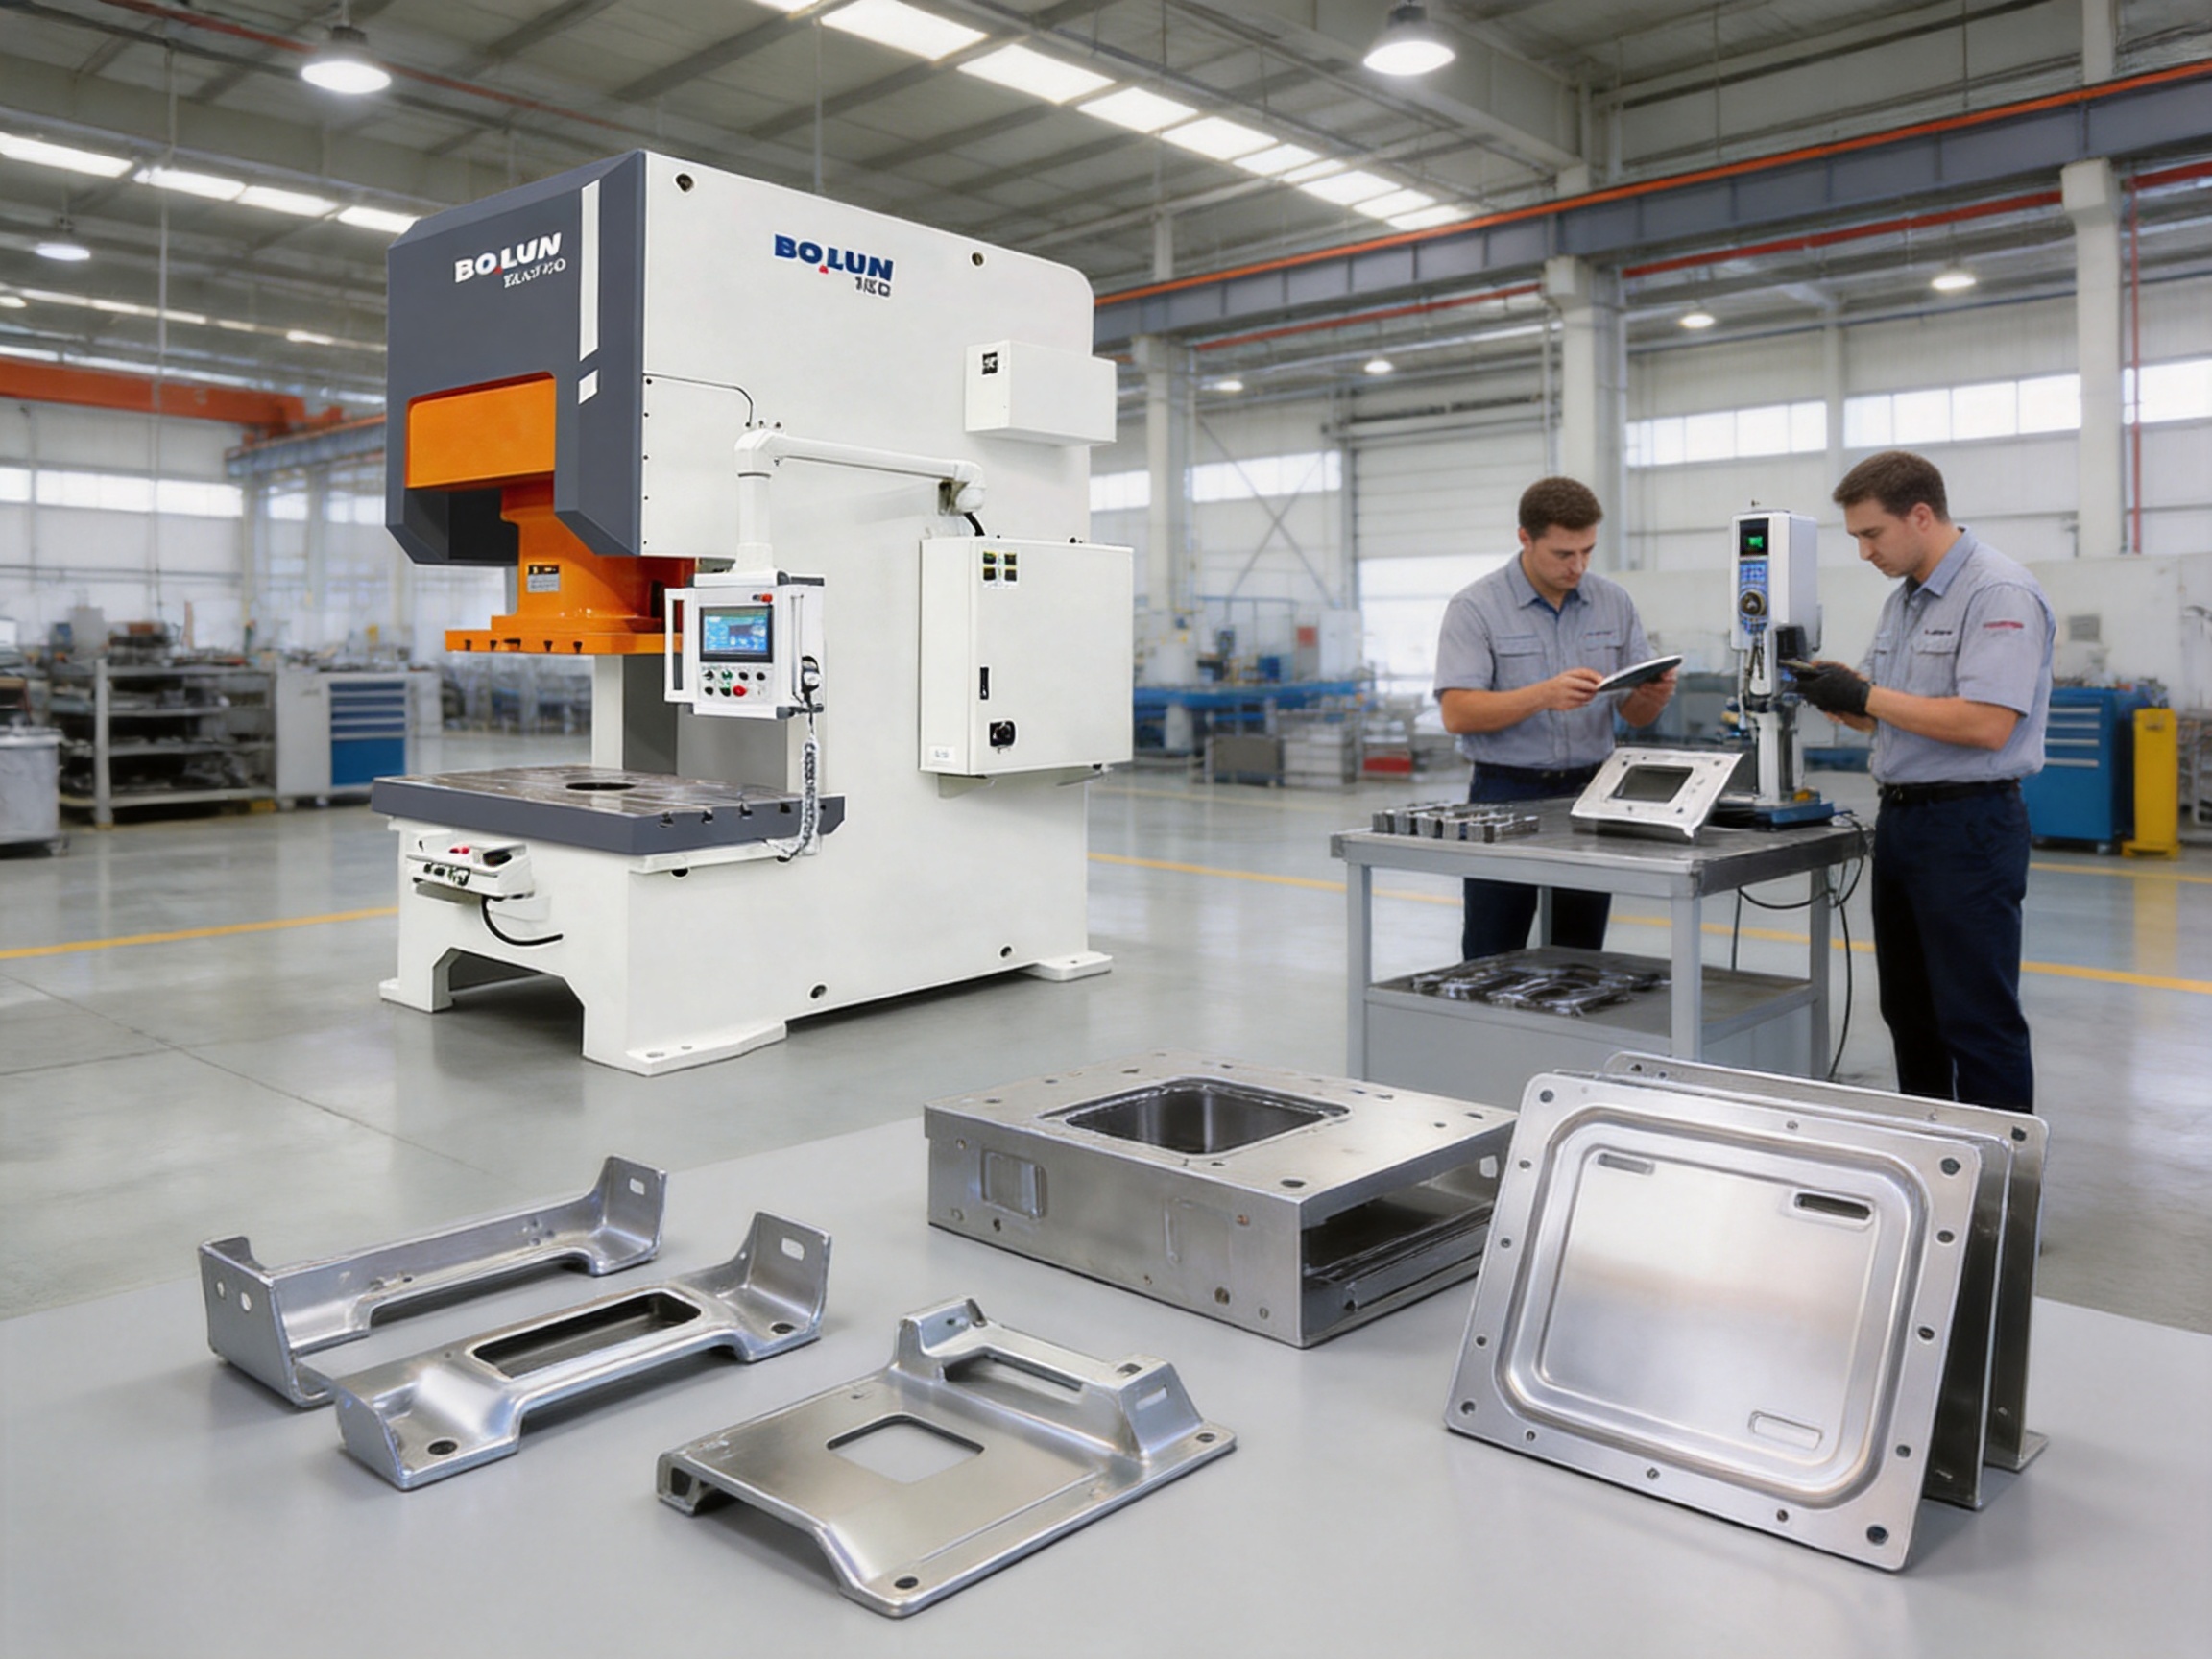
Before purchasing a press in this class, manufacturers should prepare a complete application profile. The profile should include part drawings, material grades, thickness ranges, annual production volume, die dimensions, die weight, required force, forming energy, target cycle time, automation requirements, and quality expectations.
The 1,600 kN rating should be compared with calculated peak and continuous loads. Customers should also verify eccentric load conditions, because a die may apply force away from the machine centerline. Worktable and slide dimensions should be compared with actual die plates, guide arrangements, cushions, sensors, and feeding equipment.
The 400 mm maximum die height and 100 mm adjustment range must be checked against every planned die. The 200 mm slide stroke should be evaluated in relation to material handling and forming depth. If a part requires a longer stroke or a special motion sequence, this should be discussed during technical specification.
Customers should ask about control-system functions, program storage, data access, alarm history, safety interfaces, language options, remote service capability, spare parts, and operator training. They should also confirm whether the standard machine includes the required die cushion, sensors, guarding, lubrication equipment, and automation interfaces.
Finally, total cost of ownership should be evaluated. The purchase price is only one element. Installation, foundation work, tooling, automation, training, maintenance, energy, spare parts, downtime, and technical service all influence the long-term return on investment.
Before full-scale production, manufacturers should conduct a structured validation process. The first stage is a design review to confirm that the die, material, and machine are compatible. The second stage is a controlled setup using low-speed or trial conditions where appropriate. The third stage is a production trial under representative operating parameters.
During validation, engineers should record forming force, slide motion, cushion settings, material position, part dimensions, surface quality, and cycle performance. Any alarms, unusual noise, vibration, or load deviation should be investigated before approval.
Once the process is stable, the approved motion profile and operating parameters can be stored for future use. A documented setup sheet should accompany the program and identify material, die, lubrication, inspection points, and allowable process limits.
Ongoing production control should combine tonnage monitoring with periodic dimensional inspection. Monitoring is valuable, but it should not replace direct quality checks. The strongest system uses machine data, operator observations, tooling inspection, and finished-part measurement together.
The nominal capacity is 1,600 kN. This makes the machine suitable for many medium-to-large stamping operations that require significantly more force than light and medium-duty presses.
Programmable motion means that the servo-driven slide can operate according to selected movement profiles. Users may adjust operating conditions such as speed zones, forming movement, dwell behavior, and return motion within the limits of the machine and the approved process.
The worktable measures 1,200 × 760 × 150 mm. The large table provides space for substantial dies, although actual die suitability must also be checked against weight, height, loading position, and force distribution.
The maximum listed die height is 400 mm, with a 100 mm die height adjustment range. Customers should calculate the complete closed die height and confirm compatibility before installation.
The listed speed is approximately 50 strokes per minute. Actual speed depends on the selected servo motion profile, material, die design, forming requirements, feeding system, and safety conditions.
Yes. The listed cushion capacity is 100 kN, with an 80 mm working stroke and an effective area of 540 × 350 mm. Its suitability depends on the intended die and forming operation.
Tonnage monitoring provides feedback about load conditions during operation. It can help identify abnormal force patterns caused by misfeeding, double-sheet loading, die problems, material changes, or other process deviations.
It is designed for high-load stamping applications commonly found in automotive, appliance, electrical, and general industrial manufacturing. The final suitability depends on the specific component, material, die, forming energy, and dimensional requirements.
Its principal distinction is the programmable servo motion, which provides greater flexibility in slide movement and forming control. A conventional mechanical press may be highly productive for fixed, repetitive operations, while this machine is better suited to applications requiring adaptable motion and stored process parameters.
The customer should prepare a suitable foundation, electrical supply, compressed air supply, die-handling equipment, safety clearances, material-flow arrangements, and trained personnel. Final requirements should be confirmed from the machine’s technical documentation.
The manufacturer provides non-standard customization and engineering services for special specifications and functions. Possible areas for discussion may include automation, feeding, safety systems, monitoring, die interfaces, and control requirements.
The listed punch accuracy is JIS B 6402 Level 1. Actual production accuracy also depends on installation, die precision, maintenance, material consistency, and operating conditions.
The BLAS-160 Heavy-Duty Programmable Motion Open-Type Single-Point Servo Power Press is positioned as a high-capacity forming solution for manufacturers that need force, workspace, process flexibility, and production control in one machine. Its 1,600 kN nominal capacity, 9,000 J continuous working energy, 1,200 × 760 mm worktable, 200 mm slide stroke, and approximately 50 S.P.M. operating capability provide a strong foundation for demanding stamping work.
Its most distinctive advantage is the servo-driven programmable motion system. This architecture allows manufacturers to adjust forming behavior more precisely than with a fixed-motion press. Controlled speed, programmable sequences, stored die parameters, tonnage monitoring, and HMI-based operation can improve repeatability and provide better visibility into the production process.
The machine is further supported by practical die accommodation, a 100 kN cushion system, JIS B 6402 Level 1 punch accuracy, and an open-front structure suited to manual and automated production. These features make it a versatile candidate for automotive, appliance, electrical, and general industrial applications.
The manufacturer’s integrated approach to research, design, precision processing, assembly, quality inspection, customization, and service strengthens the machine’s value as an industrial investment. For customers with demanding parts or special production requirements, the ability to work with an engineering-oriented supplier can be as important as the press specifications themselves.
As with any high-capacity stamping system, successful results depend on correct die design, material evaluation, installation, operator training, preventive maintenance, and process validation. When these factors are managed together, this heavy-duty servo power press can support stable forming, improved production consistency, and a more flexible response to modern manufacturing requirements.
1. Product technical data for the BLAS-160 Heavy-Duty Programmable Motion Open-Type Single-Point Servo Power Press.
2. JIS B 6402, Accuracy requirements and inspection principles for mechanical presses.
3. General principles of sheet-metal forming, stamping-force calculation, and die-process planning.
4. Industrial guidance on servo press motion control, tonnage monitoring, and programmable forming processes.
5. Manufacturer-provided information on precision machinery design, production management, customization, quality inspection, and after-sales service.


A buyer comparing a 45-ton open-gap press for a bracket line often receives two...
What Is a Power Press? A power press — also called a stamping press or punch pr...
Understanding Mechanical Power Presses and Their Essential Functions A mechani...
In the fields of metal forming, sheet metal fabrication, blanking, and punching,...
Two presses can both carry a 200-tonne nameplate and still produce very differe...
Power press machines are classified in two main ways: by frame construction, w...
Contact Us

topbolun@gmail.com

+86-575-83362228

+86-13735238388
+86-18667502750

+86-575-83362999

+8618667502750

No.1 Linjiang Road East, Xiaren, Jinting Town, Shengzhou City, Zhejiang Province, China
Ready to Begin?
Get in Touch

Now!

ZHEJIANG BOLUN
 English
 中文简体